

 English
 Español
 عربى

Get Social
Choose DEIF for the perfect blend of
performance and aesthetics.
 Get Free Sample
Content
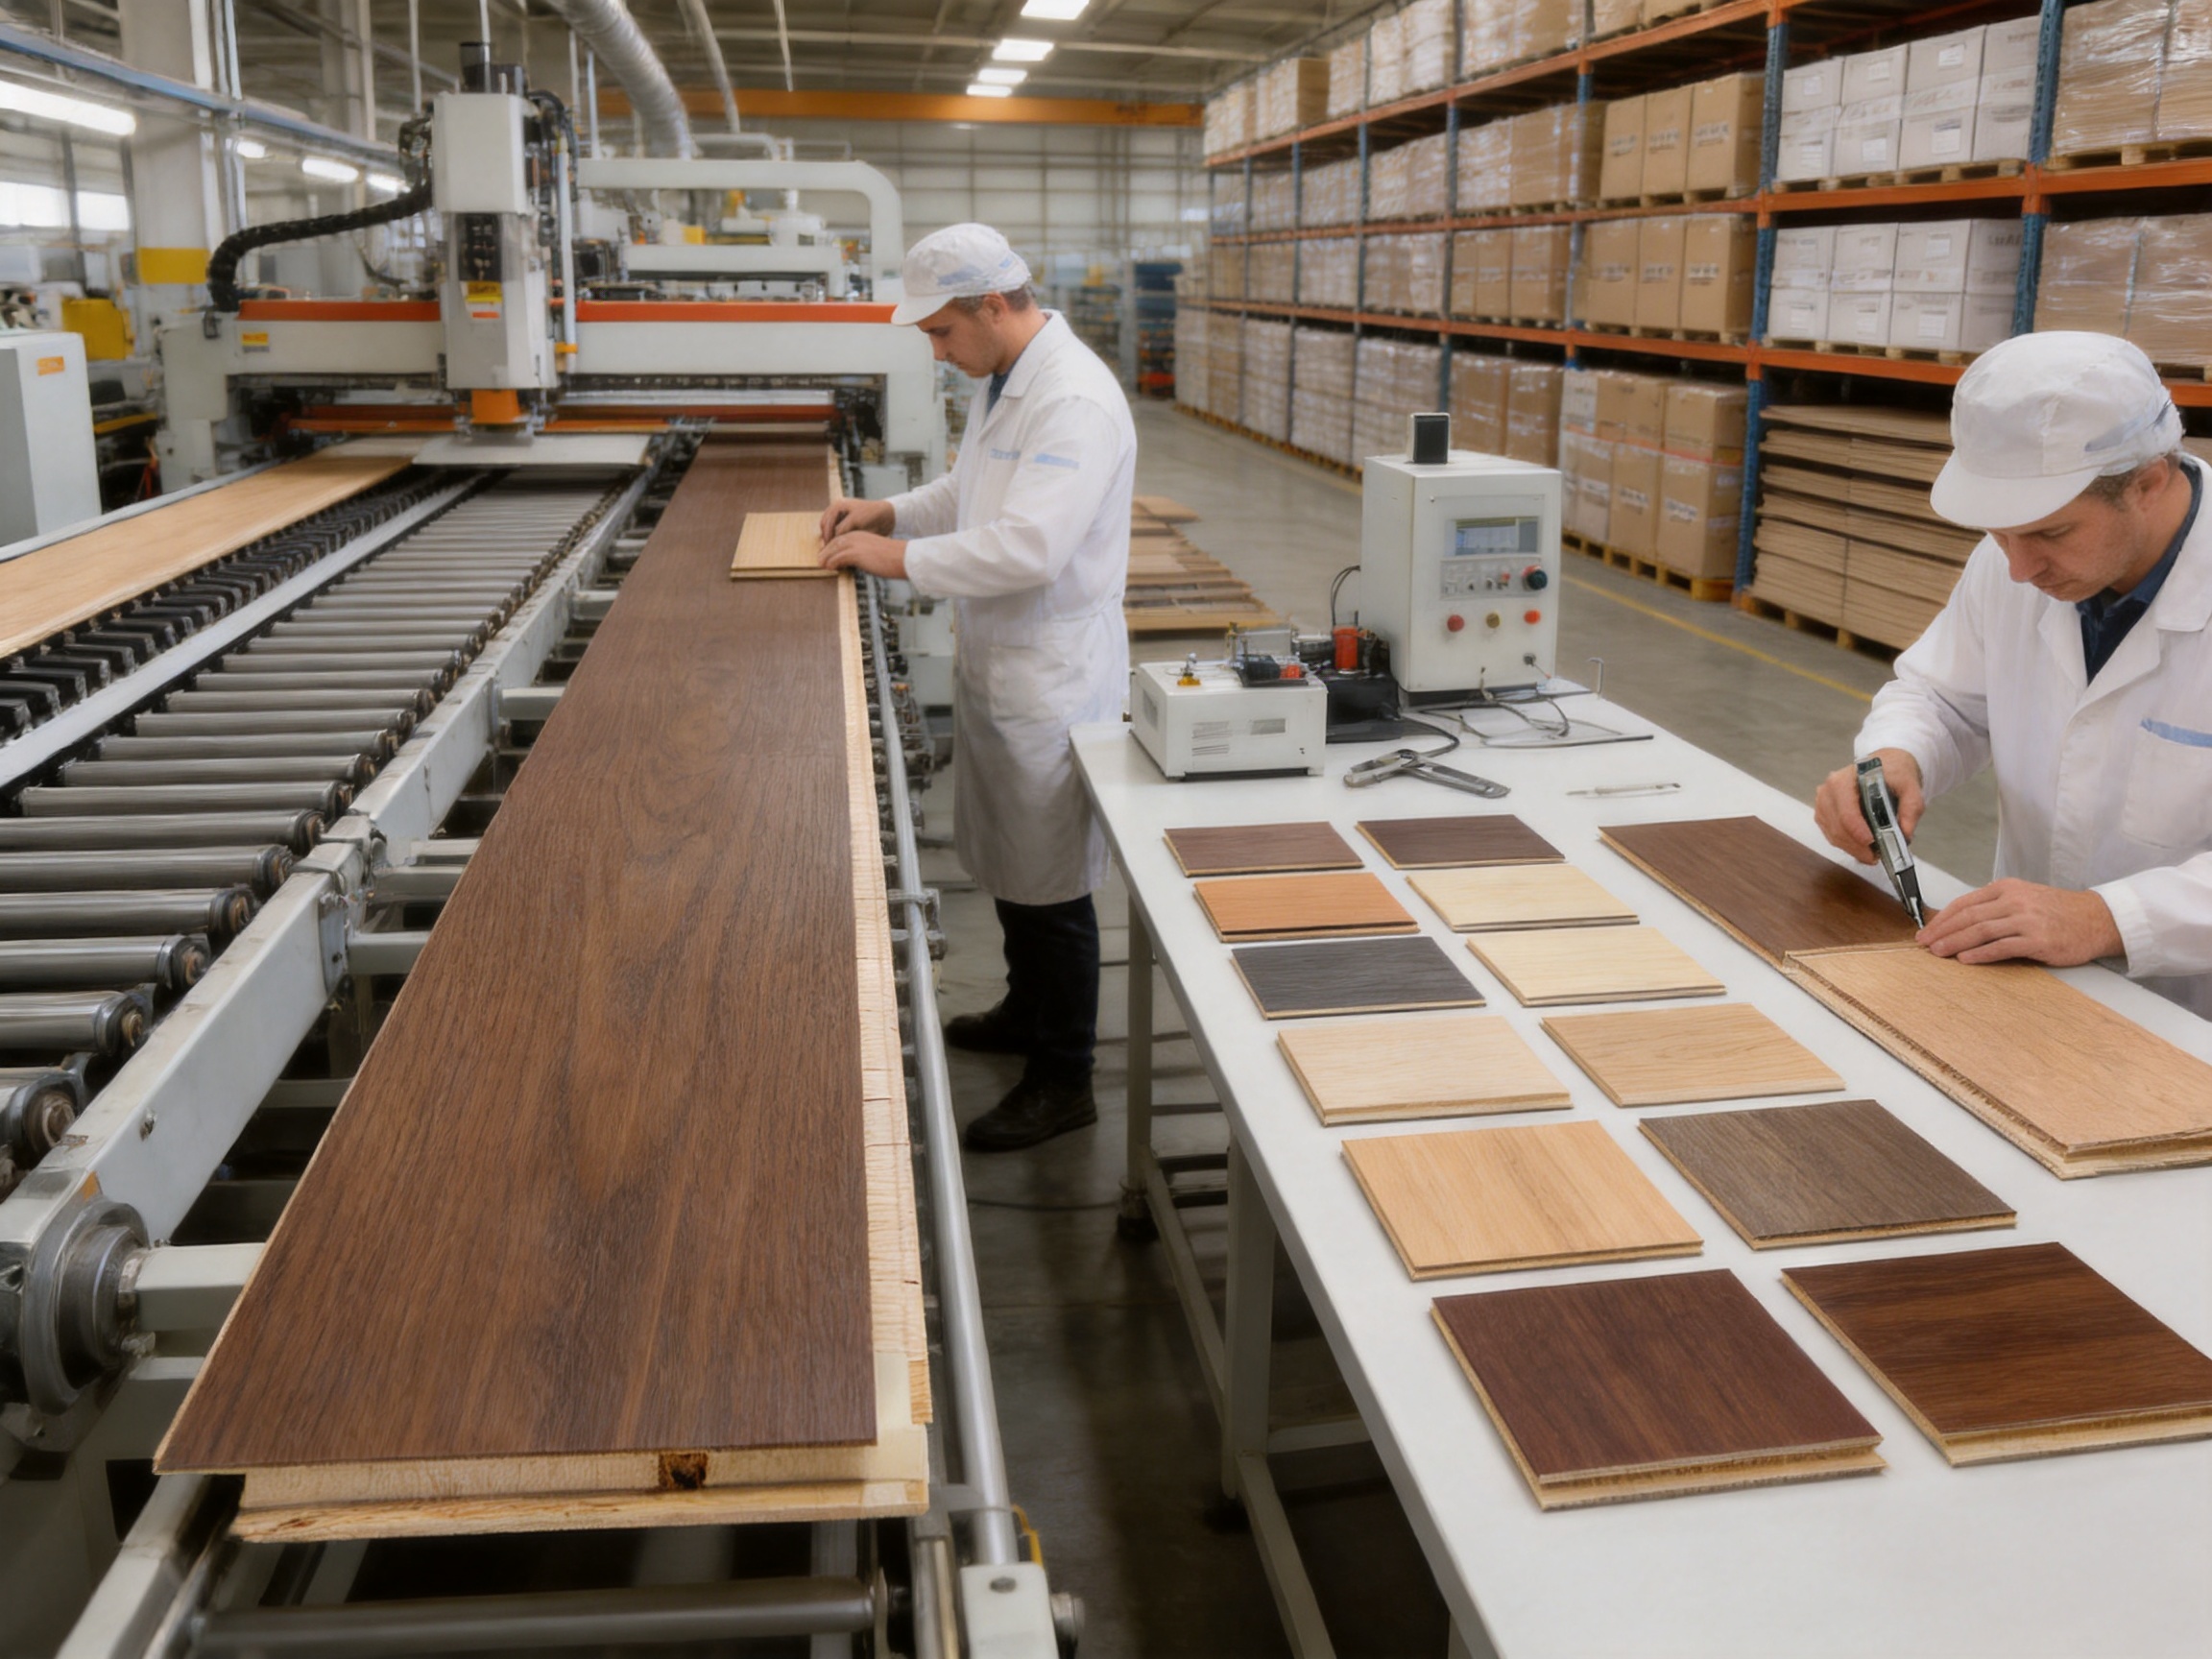
Engineered wood flooring has become a preferred surface solution for residential, commercial, and architectural interiors that require the appearance of natural timber with improved dimensional stability. Among the many available flooring formats, 3-layer interlocking engineered wood flooring offers a practical combination of authentic wood character, structural performance, installation efficiency, and design flexibility. The DC-H2306 model is developed for projects that need a dependable floor covering with natural visual appeal, customizable specifications, and compatibility with several installation methods.
Unlike conventional solid wood flooring, which is manufactured from a single direction of timber and can be more sensitive to changes in temperature and humidity, engineered flooring uses a carefully designed layered construction. The wood layers are arranged to balance one another, helping reduce the movement that can lead to warping, deformation, cracking, or visible gaps. This makes the product suitable for modern interiors where long-term appearance and reliable performance are equally important.
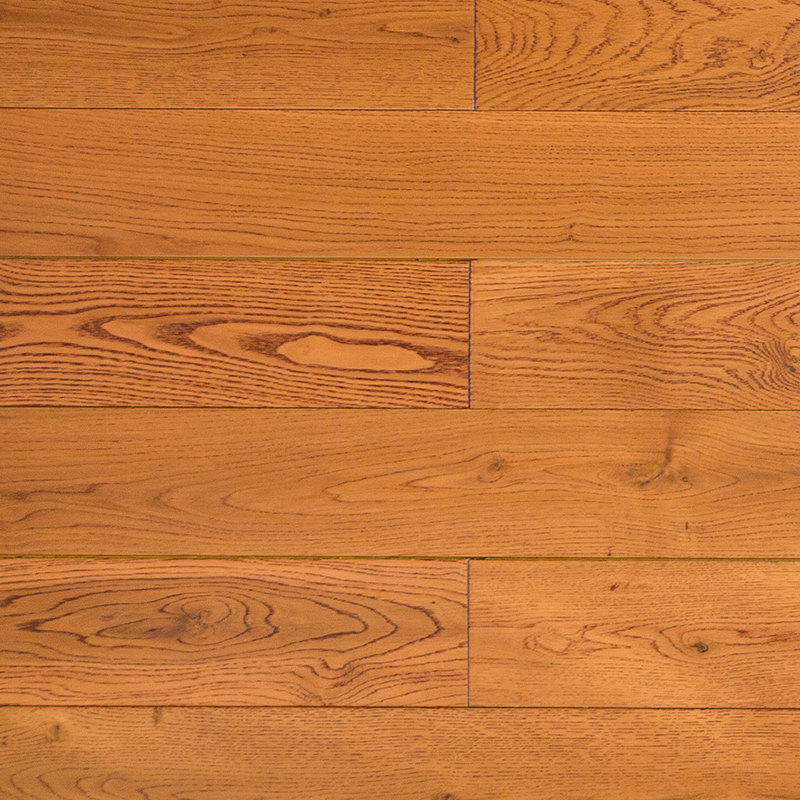
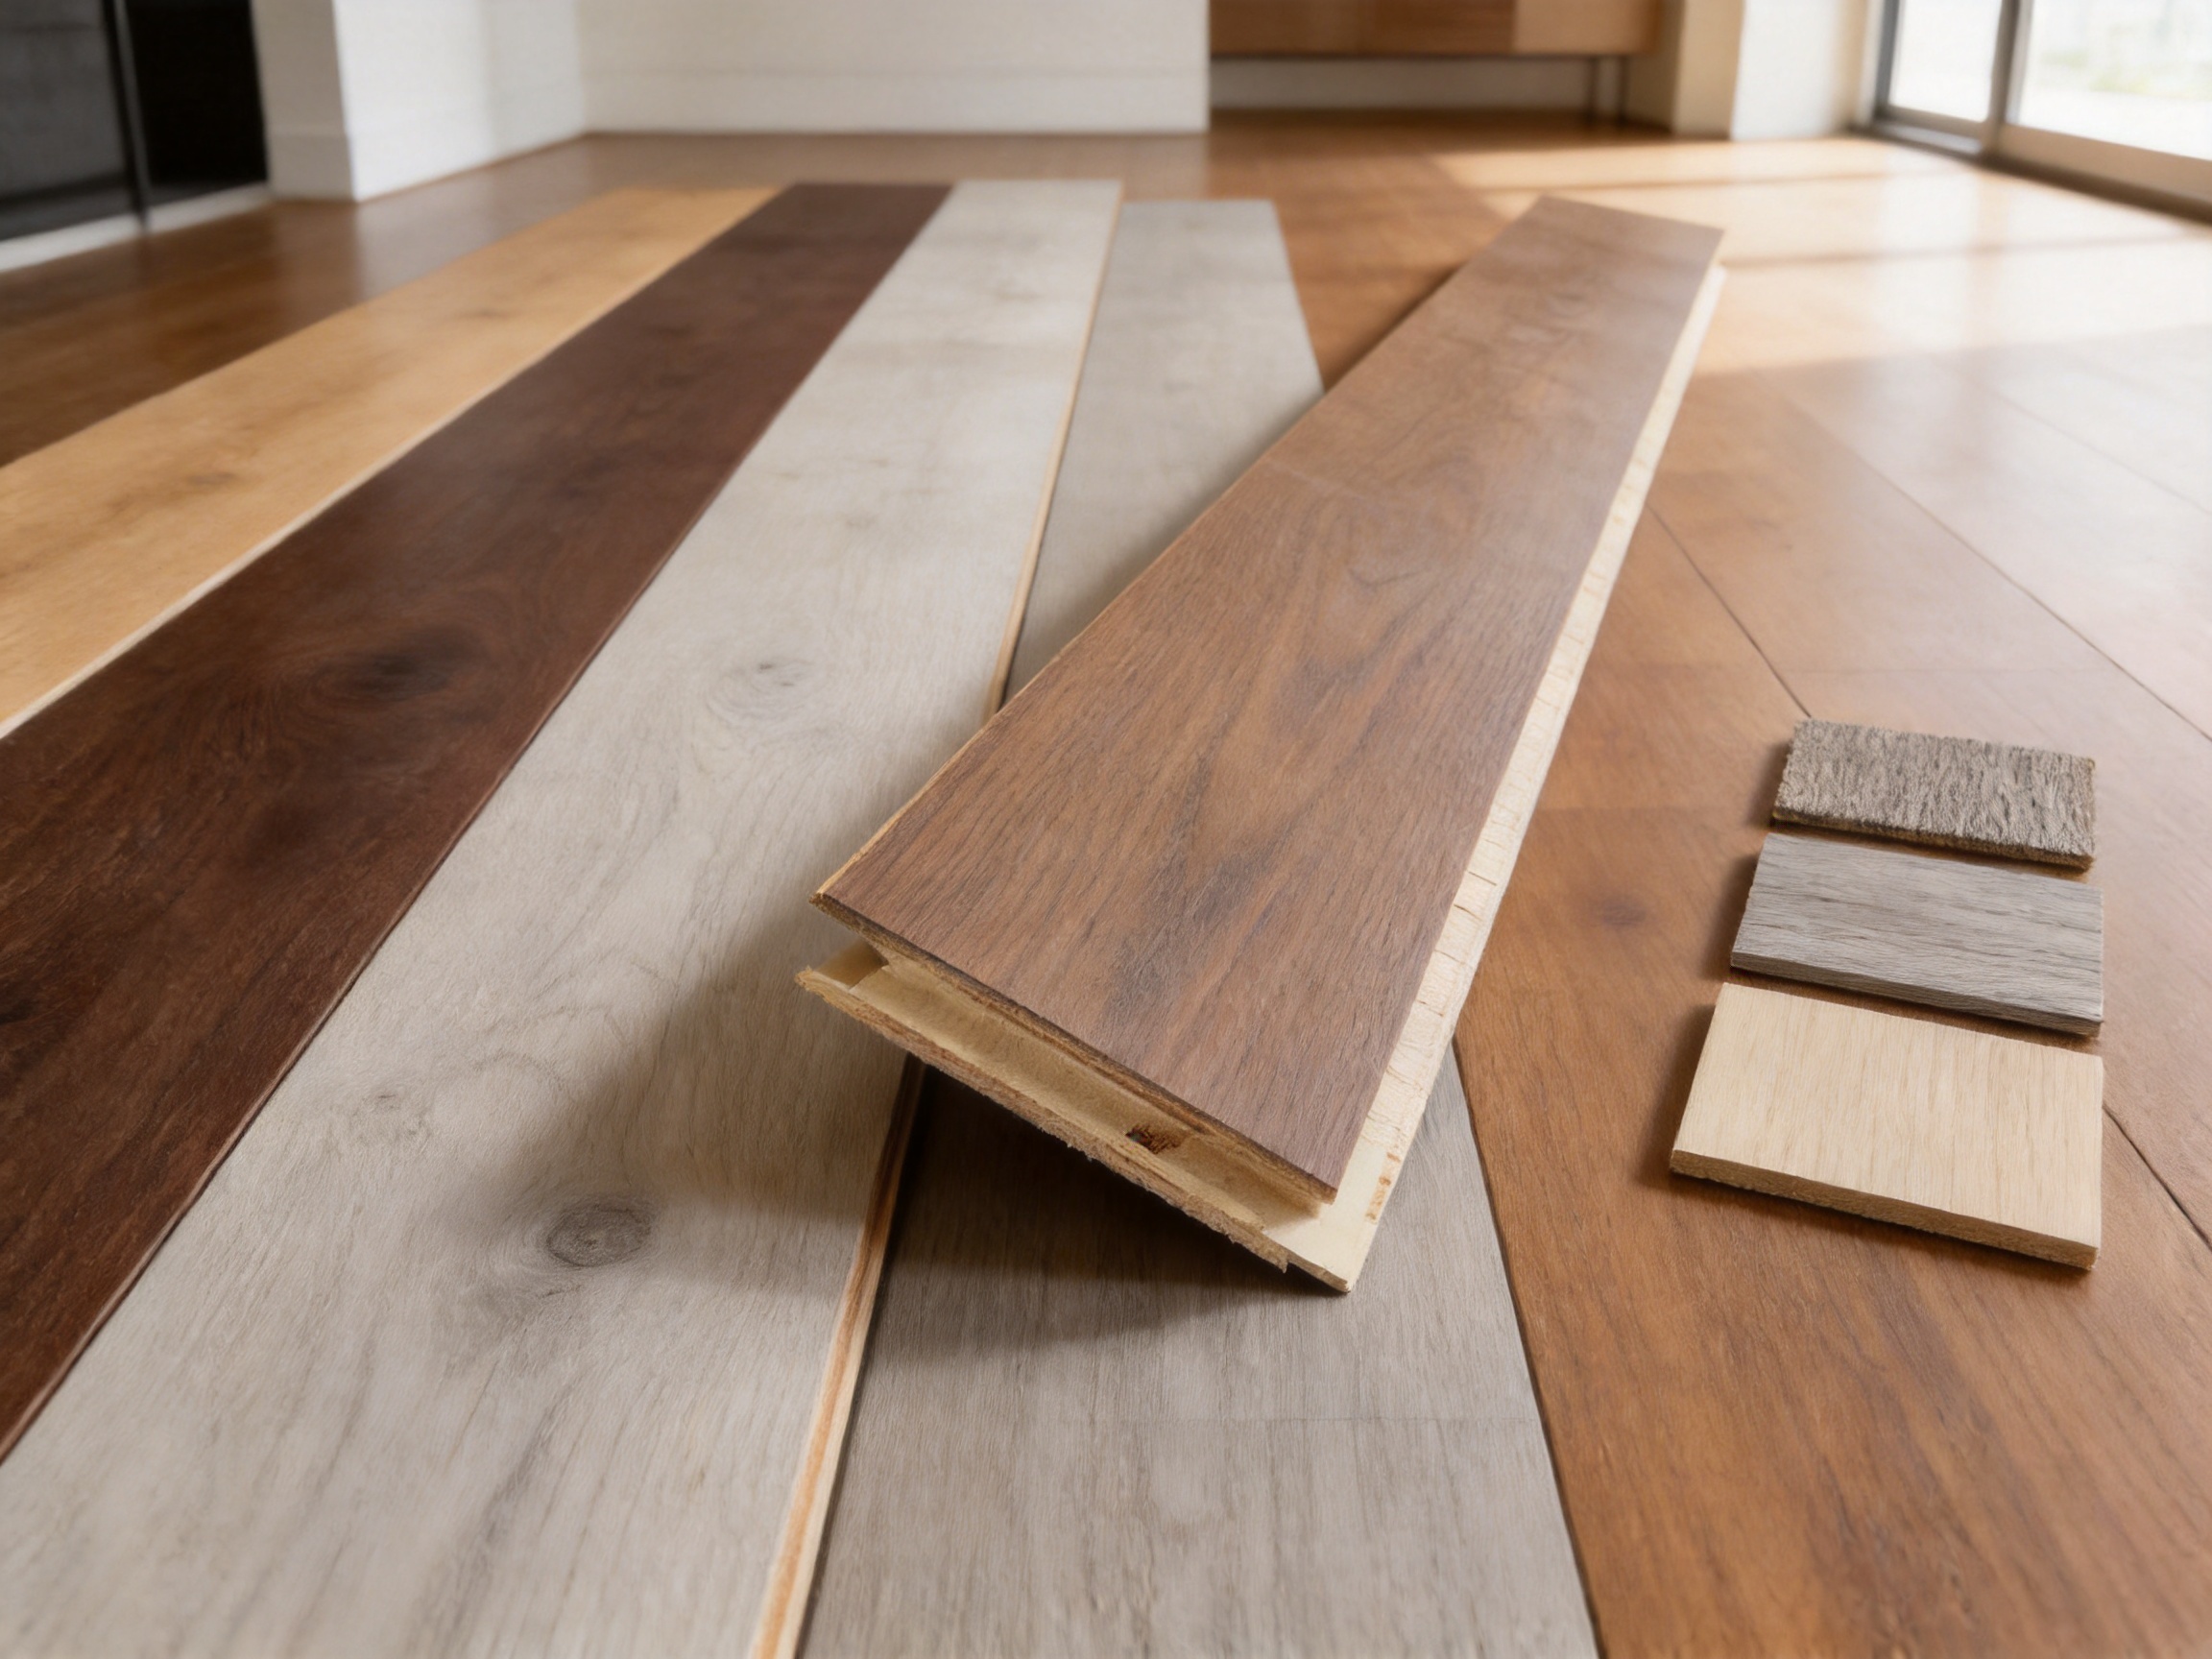
The DC-H2306 combines a natural sliced wood veneer, a three-layer spruce or pine core, a click locking system, and a customizable surface finish. Its standard format measures approximately 74.8 inches by 7.7 inches by 5/8 inch, providing a generous plank appearance while remaining manageable during transportation and installation. Customers can also select from several wood species, veneer grades, veneer thicknesses, textures, and finishing systems to create a flooring specification aligned with a particular design concept or project requirement.
Three-layer engineered wood flooring is constructed from three principal layers of wood. The visible top layer consists of a real wood veneer, while the underlying layers are positioned to improve stability and support. In the DC-H2306 construction, the core uses spruce or pine materials selected for their balance of strength, workability, and weight.
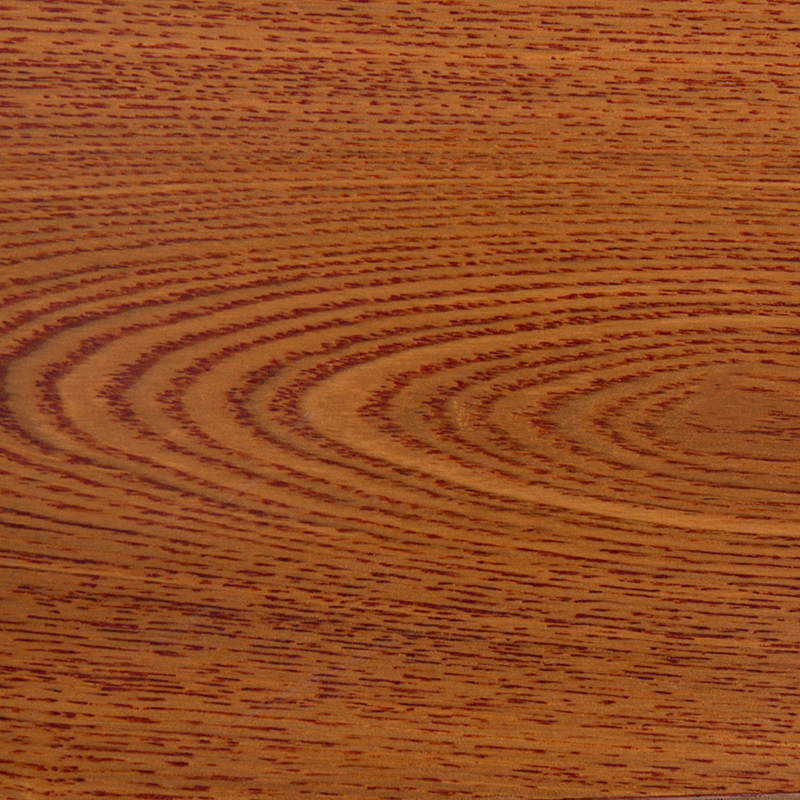
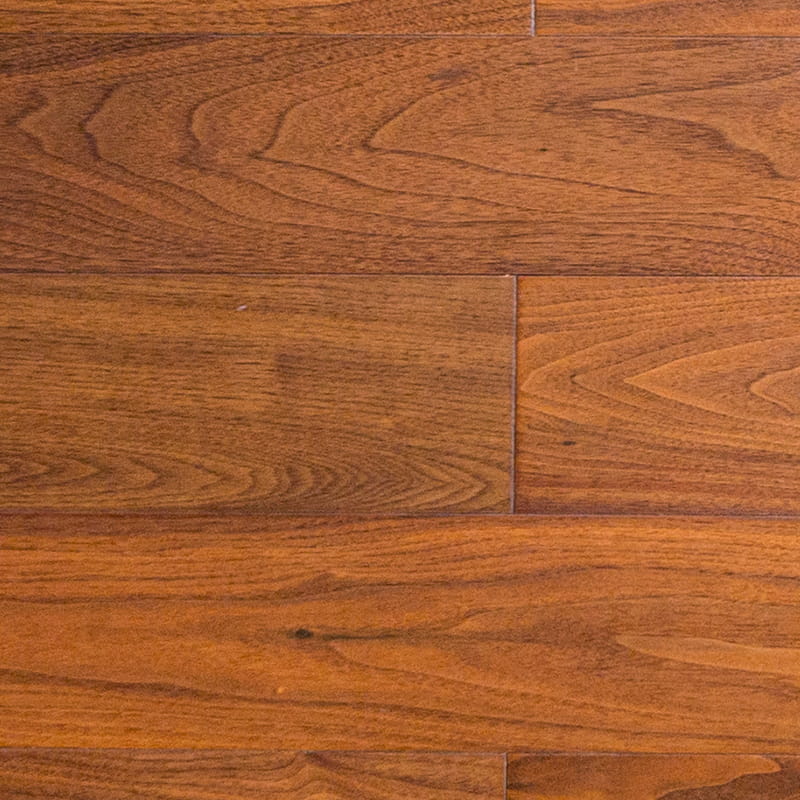
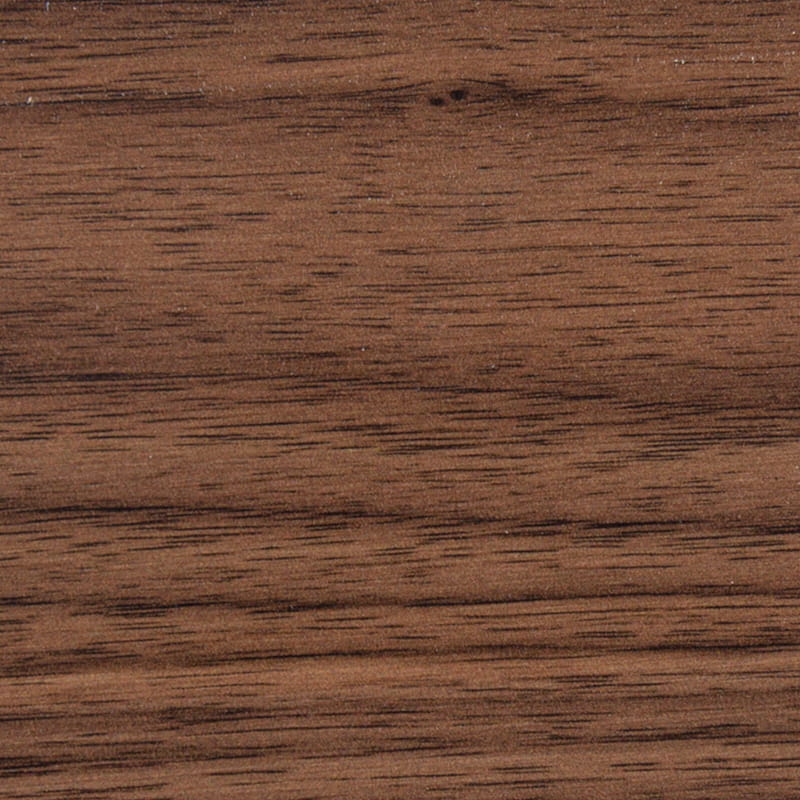
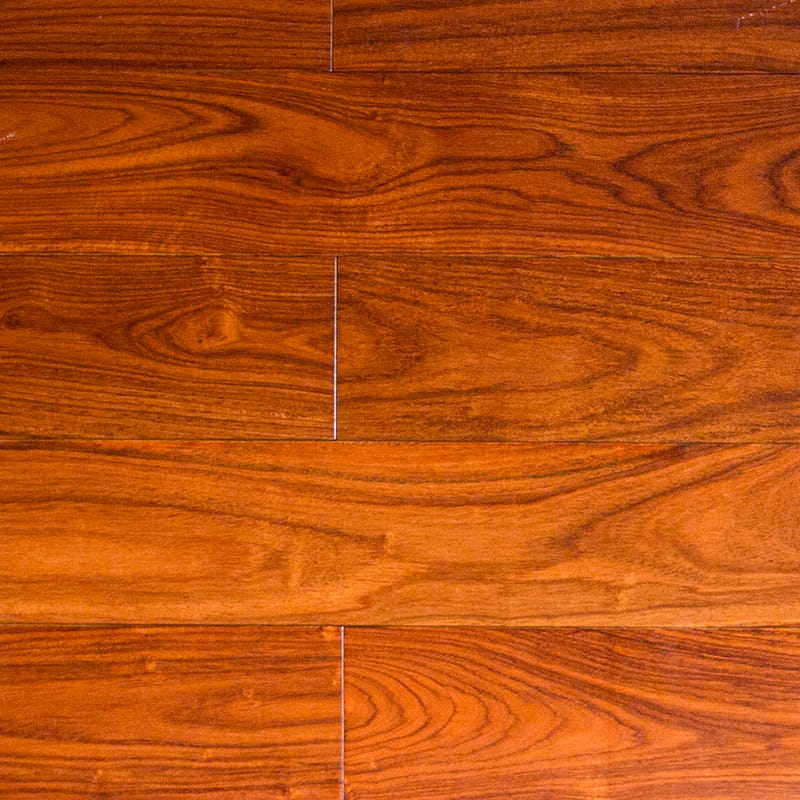
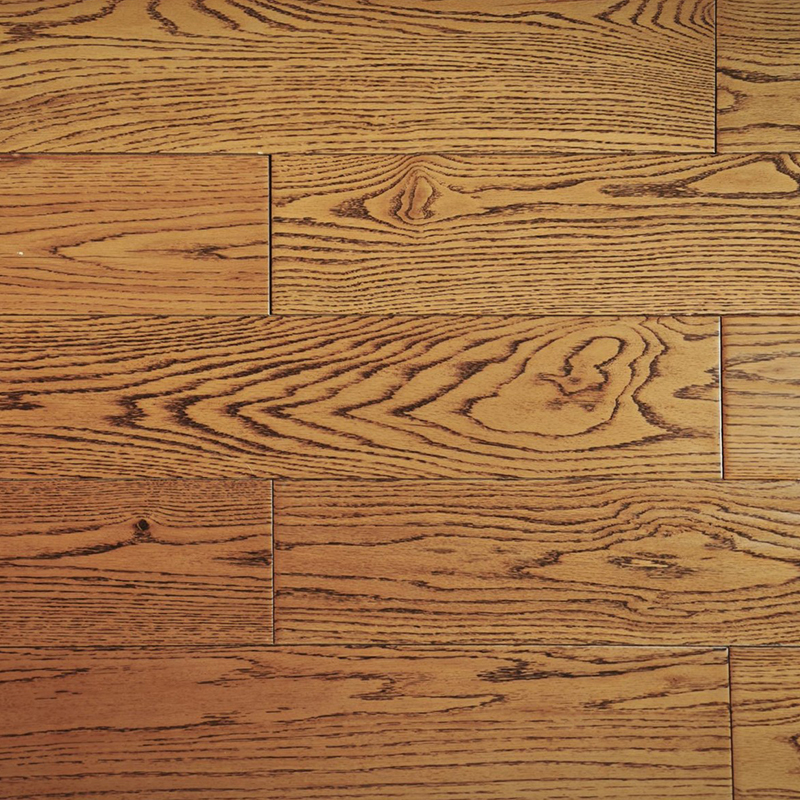
The upper veneer creates the visual identity of the floor. Depending on the selected species, the surface can display the characteristic grain and color of oak, walnut, ash, or teak. The veneer may be specified in thicknesses ranging from 2 millimeters to 6 millimeters, allowing buyers to balance budget, appearance, service expectations, and future maintenance preferences.
The central construction principle is cross-lamination. Wood naturally expands and contracts in response to environmental moisture and temperature. When individual layers are arranged in opposing directions, their movement is balanced across the board. This does not eliminate natural wood movement entirely, but it significantly improves dimensional control compared with many single-layer alternatives.
The result is a flooring product that retains the warmth and authenticity of real wood while providing a more engineered performance profile. For architects, flooring distributors, contractors, and property developers, this combination can simplify specification decisions and reduce concerns associated with installing solid timber over changing indoor environments.
A major advantage of engineered wood flooring is that it does not imitate natural wood through printing alone. The DC-H2306 uses a genuine wood veneer surface, preserving the grain direction, tonal variation, and tactile character associated with real timber. This provides a more convincing appearance than synthetic wood-look products and allows each installation to maintain a sense of natural individuality.
Oak is a popular choice for projects requiring a balanced grain, moderate variation, and broad compatibility with contemporary interiors. Walnut offers deeper brown tones and a more distinctive visual presence, making it suitable for executive offices, premium residences, hospitality settings, and statement rooms. Ash generally provides a lighter appearance with visible grain movement, while teak can contribute warm, rich tones and a refined natural character.
Because the veneer is available in multiple grades, customers can select the degree of natural variation they want. Options include AB, ABC, ABCD, and CD grades. Higher-grade selections may provide a more uniform and refined surface, while more character-oriented grades can include stronger natural variation and a more rustic appearance. This flexibility makes the product suitable for minimalist, Nordic, traditional, contemporary, and hospitality-inspired designs.
The veneer thickness is also customizable. A 2-millimeter veneer can support cost-conscious applications where the primary requirement is a genuine wood surface and stable structural performance. Thicker 3-millimeter, 4-millimeter, or 6-millimeter veneers can provide a more substantial timber appearance and may offer greater flexibility for selected future maintenance programs, subject to the chosen finish and professional assessment.
3-Layer Interlocking Quick-Installation Engineered Wood Flooring
Flooring performance depends on more than the appearance of the surface. A beautiful veneer cannot compensate for an unstable foundation, which is why the core construction is central to the DC-H2306 design. The three-layer spruce or pine structure is engineered to distribute stresses throughout the plank and reduce the risk of excessive movement.
Spruce and pine are widely used in engineered wood construction because they offer a practical balance of strength, weight, availability, and machinability. Their relatively manageable density supports efficient production and transportation, while their structural properties help create a firm substrate for the top veneer. When combined in a cross-laminated configuration, the layers work together to improve dimensional stability.
This construction is especially valuable in spaces where indoor conditions change over the year. Heating systems can reduce indoor humidity during colder months, while ventilation, air conditioning, seasonal weather, or coastal environments can create different moisture conditions. A properly manufactured engineered floor is designed to handle these normal variations more effectively than many solid wood formats.
The multilayer structure also helps reduce the likelihood of cracking and distortion caused by uneven stress. While correct acclimatization, subfloor preparation, moisture control, and installation remain essential, the engineered composition provides a stronger foundation for long-term service.
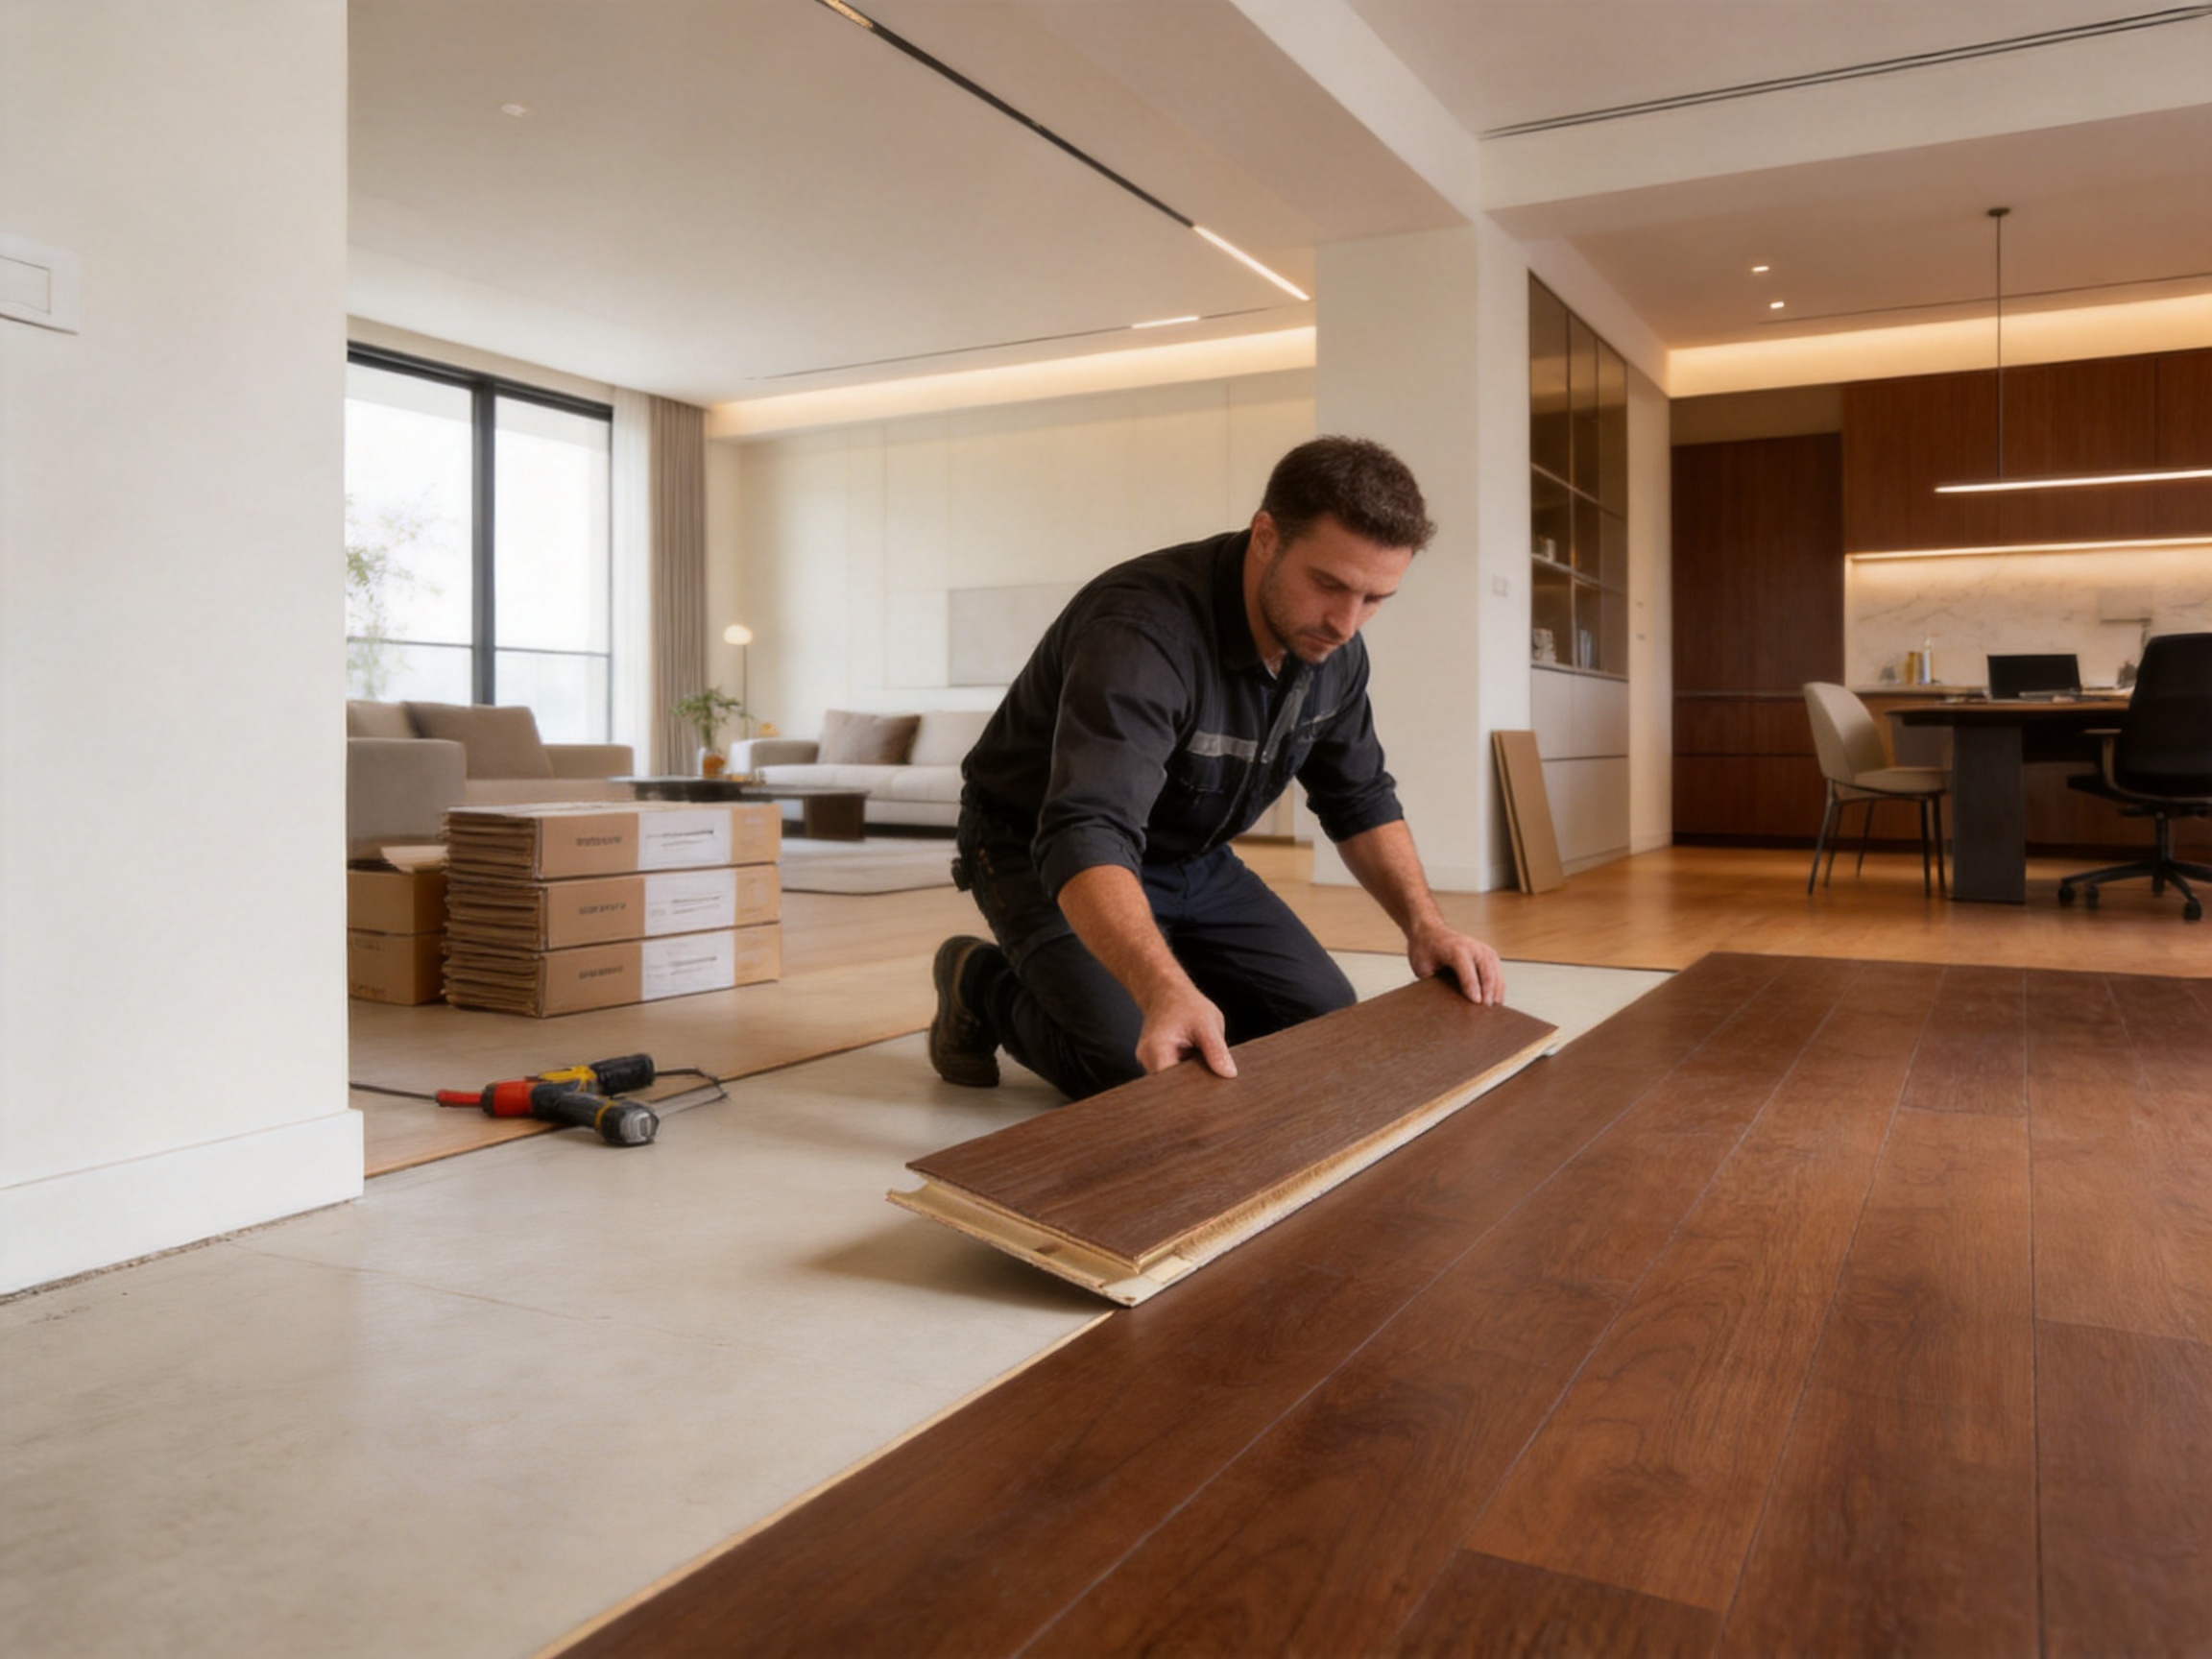
The DC-H2306 features a click system designed to support efficient installation. The interlocking profile allows adjoining planks to connect securely without relying solely on traditional nail or staple fixation. In suitable applications, the system can help reduce installation time, simplify alignment, and lower labor requirements.
Compared with flooring systems that require extensive adhesive application or complex mechanical fastening, an interlocking design can make the installation process more straightforward. Boards can be positioned, aligned, and connected in an organized sequence. The tight joint connection also helps reduce the risk of visible gaps when the subfloor is properly prepared and the product is installed according to professional guidelines.
The click system is particularly useful in renovation projects, commercial fit-outs, and residential developments where installation schedules are tightly controlled. Faster installation can help other trades begin their work sooner and may reduce disruption to building occupants. It can also support more efficient material planning because the installation team can work systematically across large areas.
Although the product is designed for quick installation, professional preparation remains important. The subfloor should be structurally sound, clean, level, and appropriately dry. Flooring should be acclimatized according to the project environment and manufacturer recommendations. Expansion allowances, room geometry, transitions, and moisture conditions should be assessed before installation begins.
One of the product’s practical strengths is its compatibility with floating, glue-down, and staple installation methods. This provides architects, contractors, and installers with greater flexibility when responding to different subfloor conditions and project specifications.
Floating installation can be appropriate for many residential and selected commercial applications. The planks are connected through the click system and installed over a suitable underlay or prepared substrate. This method can be efficient and may simplify future removal or replacement when compared with fully bonded systems.
Glue-down installation can provide a firm connection between the flooring and the subfloor. It may be selected where sound control, underfoot solidity, or project-specific performance requirements are important. The adhesive system must be compatible with the flooring, subfloor, and environmental conditions, and installation should be completed by qualified professionals.
Staple installation offers another traditional mechanical fixing option. It may be suitable for certain timber subfloors or project conditions where the installer requires direct fastening. The correct staple type, spacing, subfloor construction, and equipment settings must be confirmed before work begins.
This installation flexibility gives the DC-H2306 an advantage over products restricted to only one fitting method. Buyers can select an approach that suits the building structure, project schedule, installer expertise, acoustic objectives, and maintenance strategy.
The surface finish influences the appearance, tactile quality, cleaning routine, and wear behavior of a wood floor. The DC-H2306 can be customized with UV lacquer, UV oil, or hardwax oil finishes, allowing the product to be adapted to different visual and functional expectations.
UV lacquer forms a protective film over the wood surface. It can support resistance to everyday wear and scratching while making routine cleaning more convenient. A lacquered floor may present a consistent sheen, depending on the selected gloss level, and can be specified for projects that prioritize practical maintenance and a uniform appearance.
UV oil combines oil-based visual characteristics with a curing process that supports production efficiency and surface protection. It can preserve a natural-looking appearance while improving resistance to common household or commercial use. This type of finish may appeal to customers who want the visual warmth of an oiled floor with the consistency of a factory-applied treatment.
Hardwax oil penetrates and protects the wood while helping preserve a natural tactile sensation. It is often selected for projects where the touch and visual depth of timber are important design priorities. Hardwax oil can also support localized maintenance strategies in some applications, although all cleaning and repair procedures should follow the applicable technical guidance.
The choice of finish should consider expected traffic, cleaning practices, furniture movement, sunlight exposure, desired sheen, and the owner’s maintenance expectations. Offering several finish options is an advantage because it allows the same basic flooring construction to serve different market segments and interior styles.
In addition to wood species and finish, surface texture can significantly influence how a floor looks and feels. The DC-H2306 is available with wire-brushed, hand-scraped, or smooth-sanded textures.
Wire brushing emphasizes the natural grain by removing softer fibers from the surface. It creates a subtle tactile pattern and can enhance the visual depth of oak, ash, and other open-grained species. This option is often suitable for modern rustic, Scandinavian, coastal, and contemporary interiors.
Hand-scraped texture introduces a more artisanal appearance. Gentle variations across the surface can create the impression of individually crafted timber planks. This style may work well in traditional homes, boutique hospitality spaces, restaurants, and interiors that seek a more relaxed or character-rich atmosphere.
Smooth sanding offers a cleaner and more refined surface. It can support minimalist interiors, commercial offices, showrooms, and residential rooms where a calm visual field is preferred. The smooth profile also provides a soft, consistent touch beneath the feet.
By combining species, grade, thickness, finish, and texture, project designers can develop flooring specifications that are much more precise than selecting from a limited range of standard products. This customization is particularly valuable for private-label flooring programs, developer collections, hospitality projects, and distributor catalogs.
| Specification | DC-H2306 Standard or Available Option | Project Benefit |
| Product type | 3-layer engineered wood flooring | Balanced natural appearance and dimensional stability |
| Standard dimensions | 74.8 inches × 7.7 inches × 5/8 inch | Long, wide-plank visual effect |
| Face veneer | Oak, walnut, ash, or teak | Choice of color, grain, and design character |
| Veneer thickness | 2 mm, 3 mm, 4 mm, or 6 mm | Specification flexibility for different project budgets and uses |
| Core construction | Three-layer engineered wood | Improved resistance to deformation and cracking |
| Core material | Spruce or pine | Lightweight and structurally practical foundation |
| Veneer grades | AB, ABC, ABCD, or CD | Control over uniformity and natural character |
| Surface finishes | UV lacquer, UV oil, or hardwax oil | Different protection and visual effects |
| Surface textures | Wire brushed, hand scraped, or smooth sanded | Design adaptation for varied interior styles |
| Edge profile | Micro-bevel on all four sides | Defined plank appearance and refined transitions |
| Locking system | Click system | Efficient alignment and quick installation |
| Installation methods | Float, glue, or staple | Flexibility for different subfloors and project conditions |
Flooring in active interiors must withstand repeated walking, furniture movement, cleaning, and incidental impact. The product information identifies a seven-layer UV coating for wear and scratch resistance in general-use applications. This factory-applied coating contributes to a more durable surface and supports the floor’s ability to maintain its visual quality during everyday use.
Wear resistance is influenced by several factors, including coating composition, curing quality, veneer species, texture, furniture protection, entrance matting, cleaning practices, and traffic intensity. A well-designed finish is an important first layer of protection, but it should be supported by suitable maintenance procedures.
In residential settings, the floor can be used in living rooms, bedrooms, home offices, dining areas, and other interior spaces where natural warmth and comfort are desired. In commercial settings, it can support offices, exhibition halls, meeting areas, boutique environments, and similar spaces with moderate foot traffic.
For high-traffic commercial locations, the specification should be reviewed against the expected traffic level and project performance requirements. Entrance zones, retail corridors, hospitality lobbies, and public facilities may require additional protective measures, carefully selected finishes, planned maintenance, and appropriate cleaning equipment.
Wood flooring contributes more than a decorative surface. Its natural visual warmth can make living areas feel more welcoming, while its tactile character creates a comfortable walking experience. The DC-H2306 is suitable for living rooms, bedrooms, home offices, and other residential spaces where occupants interact with the floor every day.
The long-plank format can make a room appear more spacious and organized. Wider boards reduce the number of visible joints, while the micro-bevel on all four sides provides definition between planks. Depending on the selected grade and texture, the floor can create either a calm, uniform appearance or a more expressive natural pattern.
Light oak and ash tones can brighten rooms and complement white walls, pale textiles, natural stone, and Nordic-inspired furniture. Walnut can add depth to larger rooms, studies, libraries, and formal living areas. Teak-inspired tones can create a warm atmosphere in hospitality-style bedrooms, lounges, and premium residential interiors.
Because the floor is available in multiple surface treatments, designers can coordinate the final appearance with cabinetry, wooden doors, wall panels, furniture, and other interior woodwork. This is especially useful when a project requires a unified material palette rather than unrelated finishes from different suppliers.
Engineered wood flooring is increasingly specified for commercial environments that need a premium appearance without the installation complexity of certain solid timber systems. The DC-H2306 can be considered for offices, exhibition halls, meeting rooms, professional studios, boutique hospitality spaces, and other interiors with moderate commercial use.
In offices, natural wood can soften the visual character of workspaces and create a more comfortable atmosphere for employees and visitors. It can be used in reception areas, executive rooms, conference spaces, collaborative zones, and private offices. The selected finish and maintenance schedule should be matched to the expected level of use.
In exhibition halls and showrooms, the floor can provide a neutral yet refined background for furniture, products, artwork, and architectural displays. The choice of species and surface texture can either support the exhibits quietly or become part of the visual presentation.
In hospitality settings, engineered flooring can help create a residential sense of comfort in guest rooms, lounges, dining areas, and boutique public spaces. The click system and installation flexibility may support phased renovation programs where schedule control is important.
Architects and contractors should evaluate factors such as subfloor moisture, acoustic requirements, expected traffic, cleaning chemicals, rolling loads, sunlight, furniture movement, and local building standards before approving the product for a specific commercial application.
Solid wood flooring is manufactured from a single piece of timber, which gives it substantial material depth and a traditional appearance. However, a single-direction wood structure can respond more noticeably to changes in humidity and temperature. This may result in seasonal expansion, contraction, cupping, or gaps if environmental control and installation practices are not carefully managed.
The three-layer engineered construction provides a more balanced response to environmental changes. The opposing grain directions help control movement, making engineered flooring a practical choice for interiors where conditions are not perfectly constant. This structural advantage can be particularly relevant in modern buildings with underfloor heating, large glazed areas, air conditioning, or seasonal climate variation, subject to technical compatibility.
Engineered flooring can also reduce material consumption of premium face timber because only the visible top layer requires the selected decorative species. This allows the project to achieve the appearance of oak, walnut, ash, or teak while using a structurally efficient core beneath the veneer.
Another difference is installation flexibility. The DC-H2306 can be floated, glued, or stapled, while the click system supports efficient fitting. These options can make the product more adaptable to renovation and commercial construction schedules than some conventional solid wood systems.
Laminate flooring can provide attractive printed wood visuals and strong resistance to certain forms of surface wear. However, its decorative layer is not genuine wood, and its tactile quality may differ from natural timber. Engineered wood flooring offers an authentic veneer surface with real grain variation, natural tonal depth, and the ability to select different wood species.
Vinyl and other synthetic wood-look products can offer moisture-related advantages in selected applications, but they do not provide the same natural material composition or solid wood touch. For projects where the authenticity of timber is a central design objective, real wood veneer can create a more premium and emotionally appealing result.
The DC-H2306 therefore occupies a balanced position between solid timber and synthetic alternatives. It offers real wood character, a structurally engineered body, several installation methods, and customizable finishes. This combination can provide more design authenticity than printed products and greater dimensional control than many solid wood formats.
Product selection should always be based on the complete project brief. Areas exposed to standing water, excessive moisture, or unusual chemical conditions may require another flooring category. Engineered wood performs best when its environmental limits, installation requirements, and maintenance recommendations are properly observed.
The product is manufactured by Suzhou Dicosbo Wood Co., Ltd., a wood solutions producer with experience in wood flooring, wooden doors, and custom cabinet solutions. The company was established in 1999 and has developed production capabilities serving distributors, contractors, architects, and project customers in multiple international markets.
The manufacturing operation includes approximately 20,000 square meters of production facilities and uses German imported production lines together with automated quality control systems. This combination supports repeatable machining, consistent surface preparation, reliable profile processing, and more controlled finishing results.
Automated production is particularly valuable for engineered flooring because each plank must meet requirements for dimensional accuracy, veneer bonding, profile precision, surface preparation, finish application, and packaging. Small variations in any of these stages can affect installation efficiency or the final appearance of a completed floor.
Modern production equipment also supports the customization of sizes, colors, textures, veneer grades, and surface treatments. Customers can work with the manufacturer to develop specifications suitable for private-label collections, residential developments, commercial projects, or architectural programs.
The reported annual production capacity includes approximately 2,400,000 square meters of flooring and 5,000 sets of doors. This capacity provides a foundation for stable supply and project planning, particularly when customers require repeat orders or consistent product specifications across multiple locations.
Quality control is essential for flooring because defects can become highly visible after installation. The manufacturer applies a three-step inspection process intended to control product quality throughout production. While exact inspection criteria may vary by order and specification, a structured process generally includes checks of incoming materials, in-process manufacturing, and completed products.
Incoming material inspection can evaluate veneer quality, core material condition, moisture levels, and conformity with the approved specification. Controlling materials at the beginning helps prevent unsuitable components from entering later production stages.
In-process inspection can focus on bonding, thickness, width, length, surface preparation, click profile accuracy, edge treatment, and coating application. These checks are important because corrective action is generally more efficient before products reach final packaging.
Final inspection can assess appearance, dimensions, locking performance, finish consistency, packaging, labeling, and order conformity. A documented final check helps ensure that the products shipped to customers match the approved requirements and are ready for installation.
For distributors and project buyers, this process can reduce uncertainty during procurement. Consistent quality supports easier installation, fewer site complaints, better customer satisfaction, and stronger confidence in repeat orders.
Customization is a major strength for buyers who want more than an off-the-shelf flooring product. OEM and ODM services allow customers to develop flooring collections under their own brand or to create a project-specific design based on architectural requirements.
Customization can include wood species, veneer thickness, grade, color, surface texture, finish, dimensions, packaging, labeling, and installation profile. A distributor may request a coordinated product range with several colors and grades, while a property developer may need one distinctive floor throughout a residential project.
Architects and interior designers can also use customization to coordinate flooring with wooden doors, wall panels, cabinetry, and furniture. A unified design language can make the completed space feel more intentional and professionally resolved.
The manufacturer reports a 72-hour rapid prototyping capability. Rapid prototyping can help customers review color samples, textures, veneer selections, and surface effects before committing to larger production quantities. This can shorten decision cycles and reduce the risk of selecting a finish that does not meet the intended design outcome.
Prototype approval remains an important stage. Buyers should compare samples under the actual project lighting, review natural variation, confirm dimensions, and approve the precise surface appearance before production. Natural wood is inherently variable, so an approved sample should represent the intended range rather than a guarantee that every plank will look identical.
The product information identifies EU CE and FSC certification for general-use applications. These certifications can support international procurement and demonstrate attention to product compliance and responsible material management. The company also identifies compliance with CARB Phase 2 and ISO 9001 standards within its broader product and management system profile.
CE-related compliance is relevant to products placed on applicable European markets and indicates that the product is assessed against relevant requirements within the declared scope. FSC certification is associated with responsible forest management and supply-chain control when the relevant certified claim applies to the specific product order.
CARB Phase 2 relates to formaldehyde emissions from composite wood products in the applicable regulatory context. This is important for interior environments where material emissions are considered during specification. ISO 9001 is a quality management standard that supports systematic processes, documentation, monitoring, and continual improvement.
Buyers should confirm the exact certificate number, validity, scope, chain-of-custody status, test report, and product coverage for each project. Certification requirements can vary by country, building type, and customer specification, so documentation should be reviewed during procurement rather than assumed from general company information.
Each carton contains 10 pieces and covers approximately 2.03 square meters, or 21.85 square feet. The listed carton weight is approximately 24 kilograms. These details help distributors, contractors, and logistics teams plan storage, transportation, handling, and project delivery.
Accurate carton information supports more reliable quantity calculations. A project manager can estimate the number of cartons required from the net floor area, then add a suitable allowance for cutting, layout selection, future repairs, and installation waste. The correct allowance depends on room shape, plank length, design pattern, and installer practice.
Storage conditions are also important. Cartons should normally be kept flat, dry, protected from direct sunlight, and away from extreme temperature or humidity changes. Flooring should not be stored where water leaks, condensation, or unprotected construction activities could damage the packaging or product.
Careful handling prevents edge damage, surface abrasion, and deformation before installation. Cartons should be moved according to safe manual-handling procedures, and the flooring should remain packaged until the installation area is ready for acclimatization and fitting.
Successful installation begins before the first plank is connected. The subfloor should be inspected for flatness, strength, cleanliness, and moisture condition. Uneven areas may need correction, and contaminants such as dust, oil, paint, or loose material should be removed.
Indoor conditions should be stabilized before installation. Excessive moisture, uncontrolled heating, open windows during wet weather, or ongoing plaster and painting work can affect wood flooring. The flooring should be acclimatized in accordance with the product instructions and local project conditions.
The installer should plan the direction of the planks, starting point, joint distribution, transitions, door clearances, and expansion gaps. Long planks can create an elegant visual effect, but the layout must be carefully planned to avoid awkward short pieces or repeated joint patterns.
Micro-bevels on all four sides emphasize the individual plank format. This can enhance the appearance of the installation, especially when the surface includes wire brushing, hand scraping, or visible natural variation. The installer should protect finished areas from other trades after installation is complete.
For floating installations, the underlay must be suitable for the floor system and project requirements. For glue-down installations, the adhesive must be compatible with the flooring and subfloor. For staple installations, the fastener specification and spacing must be approved for the product construction. Professional installation is recommended for all methods.
Routine care helps preserve the appearance and performance of engineered wood flooring. Soft cleaning tools should be used for regular surface cleaning, and loose dirt should be removed before it can act as an abrasive underfoot. Dry dust mops, soft brushes, and vacuum cleaners with suitable floor attachments are generally preferable to aggressive tools.
Excessive water should be avoided. Wood-based flooring is not designed to remain wet, and standing liquid can enter joints or affect the substrate. Spills should be wiped promptly with a clean, slightly damp cloth, followed by drying when necessary.
Harsh chemical cleaners, abrasive powders, steam equipment, and unsuitable polishes may damage the finish. Cleaning products should be selected according to the specific surface treatment, whether UV lacquer, UV oil, or hardwax oil.
Protective pads should be installed beneath furniture legs. Heavy furniture should be lifted rather than dragged across the floor. Entrance mats can reduce the amount of grit and moisture brought indoors, while rugs may be used in suitable areas provided they do not trap moisture or discolor the finish.
Regular inspection of interlocking joints can help identify movement, damage, or developing gaps at an early stage. Heavy objects should not remain concentrated in one area for extended periods unless the floor and subfloor have been assessed for the expected load.
For distributors, the DC-H2306 offers a combination of recognizable product benefits and broad customization potential. The natural veneer surface provides a strong market story, while the three-layer construction and click system address practical concerns that customers often raise during product selection.
The range of wood species, grades, textures, and finishes makes it possible to create product families rather than relying on one fixed appearance. A distributor can offer light, medium, and dark tones; smooth and textured surfaces; and different grades for value-oriented and premium customer segments.
The standard carton configuration and documented dimensions simplify logistics planning. International compliance information can support product registration and project submissions, while OEM and ODM services enable buyers to develop differentiated collections instead of competing only on identical catalog products.
For contractors, installation flexibility can help match the product to different site conditions. The click system supports efficient fitting, while floating, glue, and staple methods allow the installer to choose a suitable approach based on the subfloor and project requirements.
For architects, the authentic wood surface and customizable specification provide design freedom. The product can coordinate with doors, cabinets, wall finishes, and other interior woodwork from the same manufacturer, helping simplify material selection for complete interior programs.
Engineered wood flooring can support more efficient use of decorative timber because the premium species is concentrated in the visible veneer rather than used throughout the full thickness of each plank. This construction can provide the visual benefits of selected wood species while using the core material strategically.
The long service potential of a well-maintained floor also supports responsible interior design. Durable materials can reduce the frequency of replacement, minimize disruption, and preserve the value of the original installation. Actual service life depends on traffic, maintenance, environmental control, installation quality, and the selected finish.
FSC-related certification information may provide additional support for buyers concerned with responsible forestry and supply-chain transparency. Customers should confirm the specific certified claim for the ordered material and retain the relevant documentation for project records.
Sustainable specification should consider the full product life cycle. This includes material sourcing, manufacturing efficiency, packaging, transportation, installation waste, cleaning requirements, maintenance, repair, and eventual replacement. A flooring product is most successful when its environmental objectives are aligned with realistic building use and long-term care.
The first step is to define the application. Residential bedrooms may prioritize tactile comfort and visual warmth, while offices and exhibition spaces may require greater attention to traffic, cleaning, and furniture movement. The intended use should guide the finish, texture, grade, and installation method.
The second step is to select the visual direction. Buyers should choose the wood species, color range, veneer grade, texture, and plank format. Samples should be reviewed in the intended lighting and placed beside other materials, including cabinetry, doors, paint, stone, and textiles.
The third step is to confirm the structural specification. Veneer thickness, core composition, dimensions, locking profile, edge treatment, and installation method should be recorded in the project documentation. Any variation from the standard DC-H2306 specification should be approved before production.
The fourth step is to review compliance and testing documentation. The customer should confirm the applicable certification, emissions requirements, quality records, and technical information for the destination market.
The final step is to plan delivery and installation. Carton quantities, waste allowance, storage conditions, acclimatization, subfloor preparation, expansion provisions, and protection after installation should be included in the project schedule.
The main advantage is the combination of a genuine natural wood surface with a cross-laminated core designed to improve dimensional stability. The structure helps reduce movement, warping, and cracking compared with many single-layer wood flooring products.
Yes. The product uses a natural sliced wood veneer surface. Available face species include oak, walnut, ash, and teak, subject to the selected specification and order confirmation.
Yes. Available veneer thickness options include 2 millimeters, 3 millimeters, 4 millimeters, and 6 millimeters. The appropriate thickness should be selected according to the project’s appearance, budget, maintenance, and service requirements.
The product can be customized with UV lacquer, UV oil, or hardwax oil. Each finish offers a different balance of appearance, tactile character, maintenance expectations, and surface protection.
Yes. The DC-H2306 uses a click system that supports efficient plank connection and quick installation when the subfloor and site conditions are properly prepared.
Yes. The listed installation methods include floating, glue-down, and staple installation. The most suitable method depends on the subfloor, building conditions, acoustic requirements, and professional installation recommendations.
It is suitable for living rooms, bedrooms, home offices, offices, exhibition halls, meeting areas, and similar spaces with residential or moderate commercial traffic. The specification should be reviewed carefully for areas with unusual moisture, heavy rolling loads, or very high traffic.
Use soft cleaning tools and remove dust and grit regularly. Avoid excessive water, abrasive cleaners, steam equipment, and harsh chemicals. Cleaning products should be compatible with the selected surface finish.
Yes. OEM and ODM customization is available. Customers may discuss dimensions, wood species, grades, colors, textures, finishes, packaging, labeling, and other product details with the manufacturer.
The product information identifies EU CE and FSC certification for general-use applications. The company also reports CARB Phase 2 and ISO 9001 compliance within its broader quality and product profile. Buyers should request current documents that specifically cover the ordered product and destination market.
The listed packing information indicates 10 pieces per carton, covering approximately 2.03 square meters or 21.85 square feet, with an approximate carton weight of 24 kilograms.
Compatibility should be confirmed for the specific project, heating system, installation method, and product specification. Temperature limits, moisture control, acclimatization, subfloor preparation, and expansion requirements must be reviewed before installation.
3-layer interlocking engineered wood flooring provides a balanced solution for projects seeking authentic timber character, reliable dimensional performance, and efficient installation. The DC-H2306 combines a natural wood veneer with a spruce or pine cross-laminated core, a click-locking system, a four-sided micro-bevel, and several surface treatment options.
Its advantages over many competing formats include genuine wood appearance, improved structural stability compared with many solid wood alternatives, greater authenticity than printed synthetic products, and broader installation flexibility. The availability of oak, walnut, ash, and teak veneers, together with multiple grades, thicknesses, textures, and finishes, allows the product to serve a wide range of architectural and commercial design requirements.
The manufacturer strengthens the product offering through German imported production lines, automated quality control, a three-step inspection process, rapid prototyping, OEM and ODM customization, international compliance support, and substantial production capacity. These capabilities are valuable for distributors, contractors, architects, developers, and interior brands that require both design freedom and dependable supply.
When the product is properly selected, installed, protected, and maintained, it can provide a warm, durable, and visually refined surface for residential and moderate commercial interiors. Its combination of natural material quality and engineered performance makes it a practical choice for contemporary flooring programs focused on stability, customization, and long-term design value.
1. Product specification sheet for DC-H2306 three-layer engineered wood flooring.
2. Manufacturer-provided technical information covering veneer options, core construction, surface finishes, dimensions, packaging, and installation methods.
3. General principles of engineered wood flooring construction, cross-lamination, moisture response, and dimensional stability.
4. General guidance on wood flooring installation, subfloor preparation, acclimatization, cleaning, and maintenance.
5. General information concerning CE marking, FSC chain-of-custody principles, CARB Phase 2 emissions requirements, and ISO 9001 quality management systems.
6. Manufacturer profile and production capability information for wood flooring, wooden doors, and custom cabinet solutions.
We provide customers with sustainable and eco-friendly
engineered wood solutions and services.
Choose DEIF for the perfect blend of
performance and aesthetics.
