

 English
 Español
 عربى

Get Social
Choose DEIF for the perfect blend of
performance and aesthetics.
 Get Free Sample
Content
Wood flooring has become an important design element in modern residential, hospitality, retail, and commercial interiors. Beyond covering a floor, a well-designed wood surface contributes warmth, visual balance, acoustic comfort, and a sense of natural quality. The 3-Layer Light Brown Mountain Grain Lock DIV Engineered Wood Flooring, product code DF-T1225, is developed to meet these expectations through a combination of authentic wood appearance, structural stability, installation efficiency, and flexible customization.
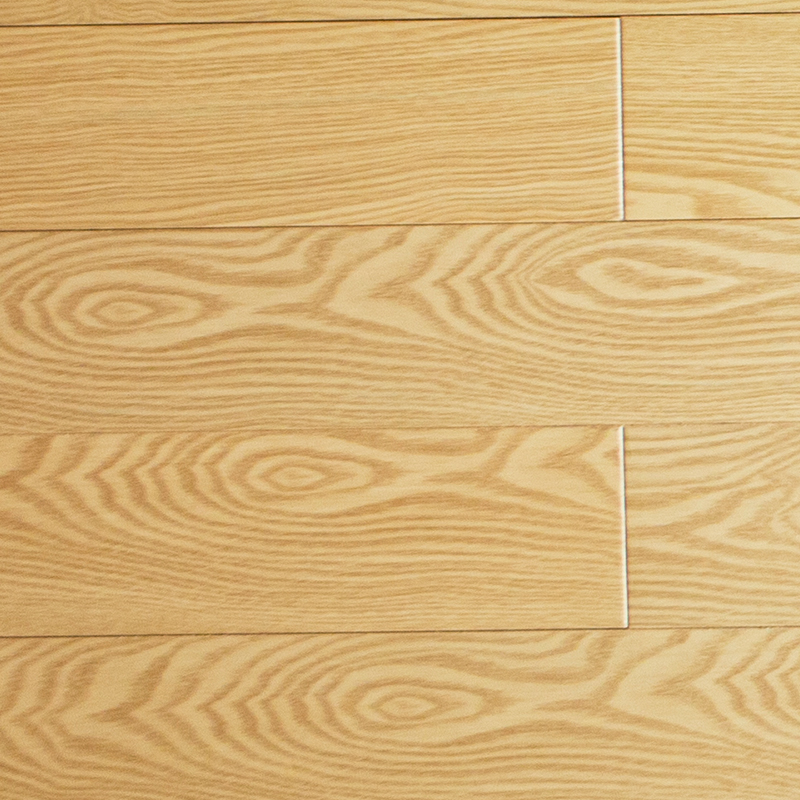
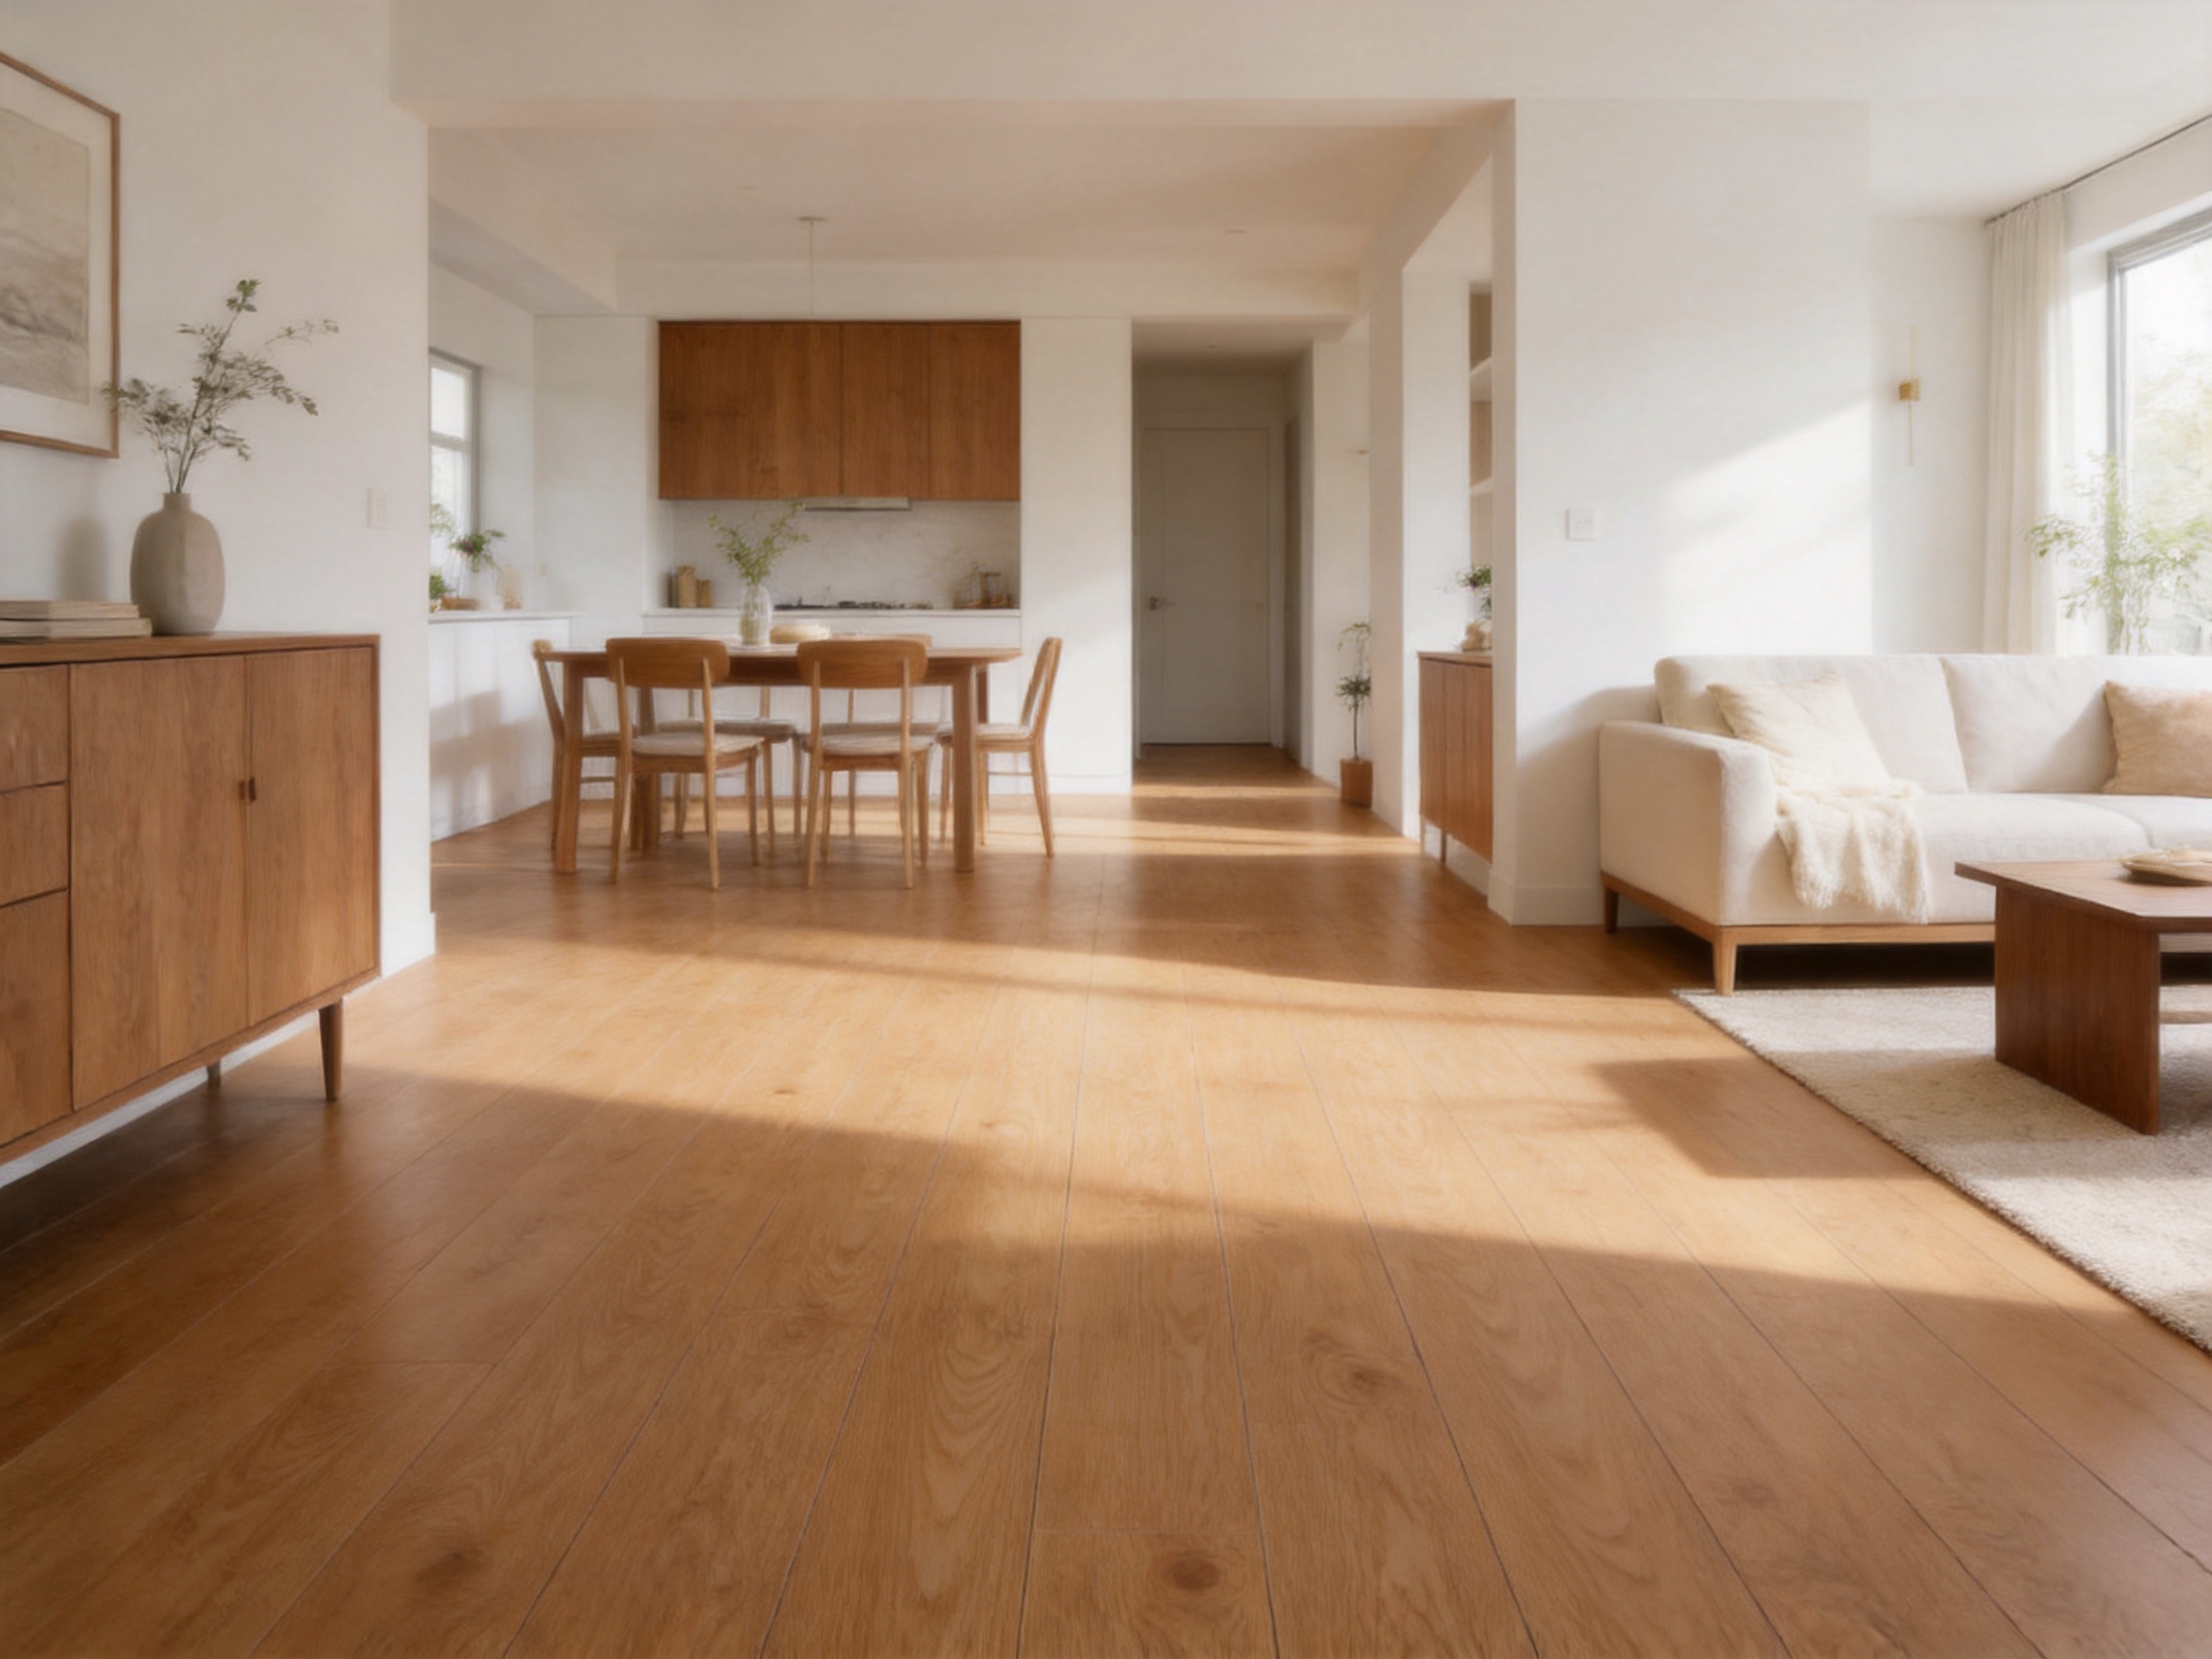
This flooring features a light brown mountain grain appearance inspired by naturally patterned oak. Its calm color and flowing grain create a warm, inviting atmosphere without overwhelming a room’s other design elements. The product is especially suitable for Nordic, Japanese, contemporary, rustic, and transitional interiors, where natural materials and understated colors are central to the overall design language.
At the same time, the flooring is engineered for practical performance. Its three-layer spruce or pine construction helps reduce the movement commonly associated with solid wood products. A natural sliced wood veneer provides the visual character of real timber, while a multi-layer surface finishing system helps improve resistance to everyday wear and scratching. The Lock DIV click system supports fast installation and can help shorten renovation schedules for both private and commercial projects.
For distributors, contractors, architects, developers, and homeowners, DF-T1225 offers a balanced alternative to conventional solid wood flooring and less authentic decorative flooring products. It provides the natural appearance expected from premium wood while offering a more controlled structure, multiple installation methods, and broad customization options.
The 3-Layer Light Brown Mountain Grain Lock DIV Engineered Wood Flooring is part of the three-layer engineered flooring category. Its standard format is 48.0 inches long, 6.5 inches wide, and 5/8 inch thick. Each carton contains 10 pieces and covers approximately 21.85 square feet, or 2.03 square meters. The approximate carton weight is 24 kilograms.
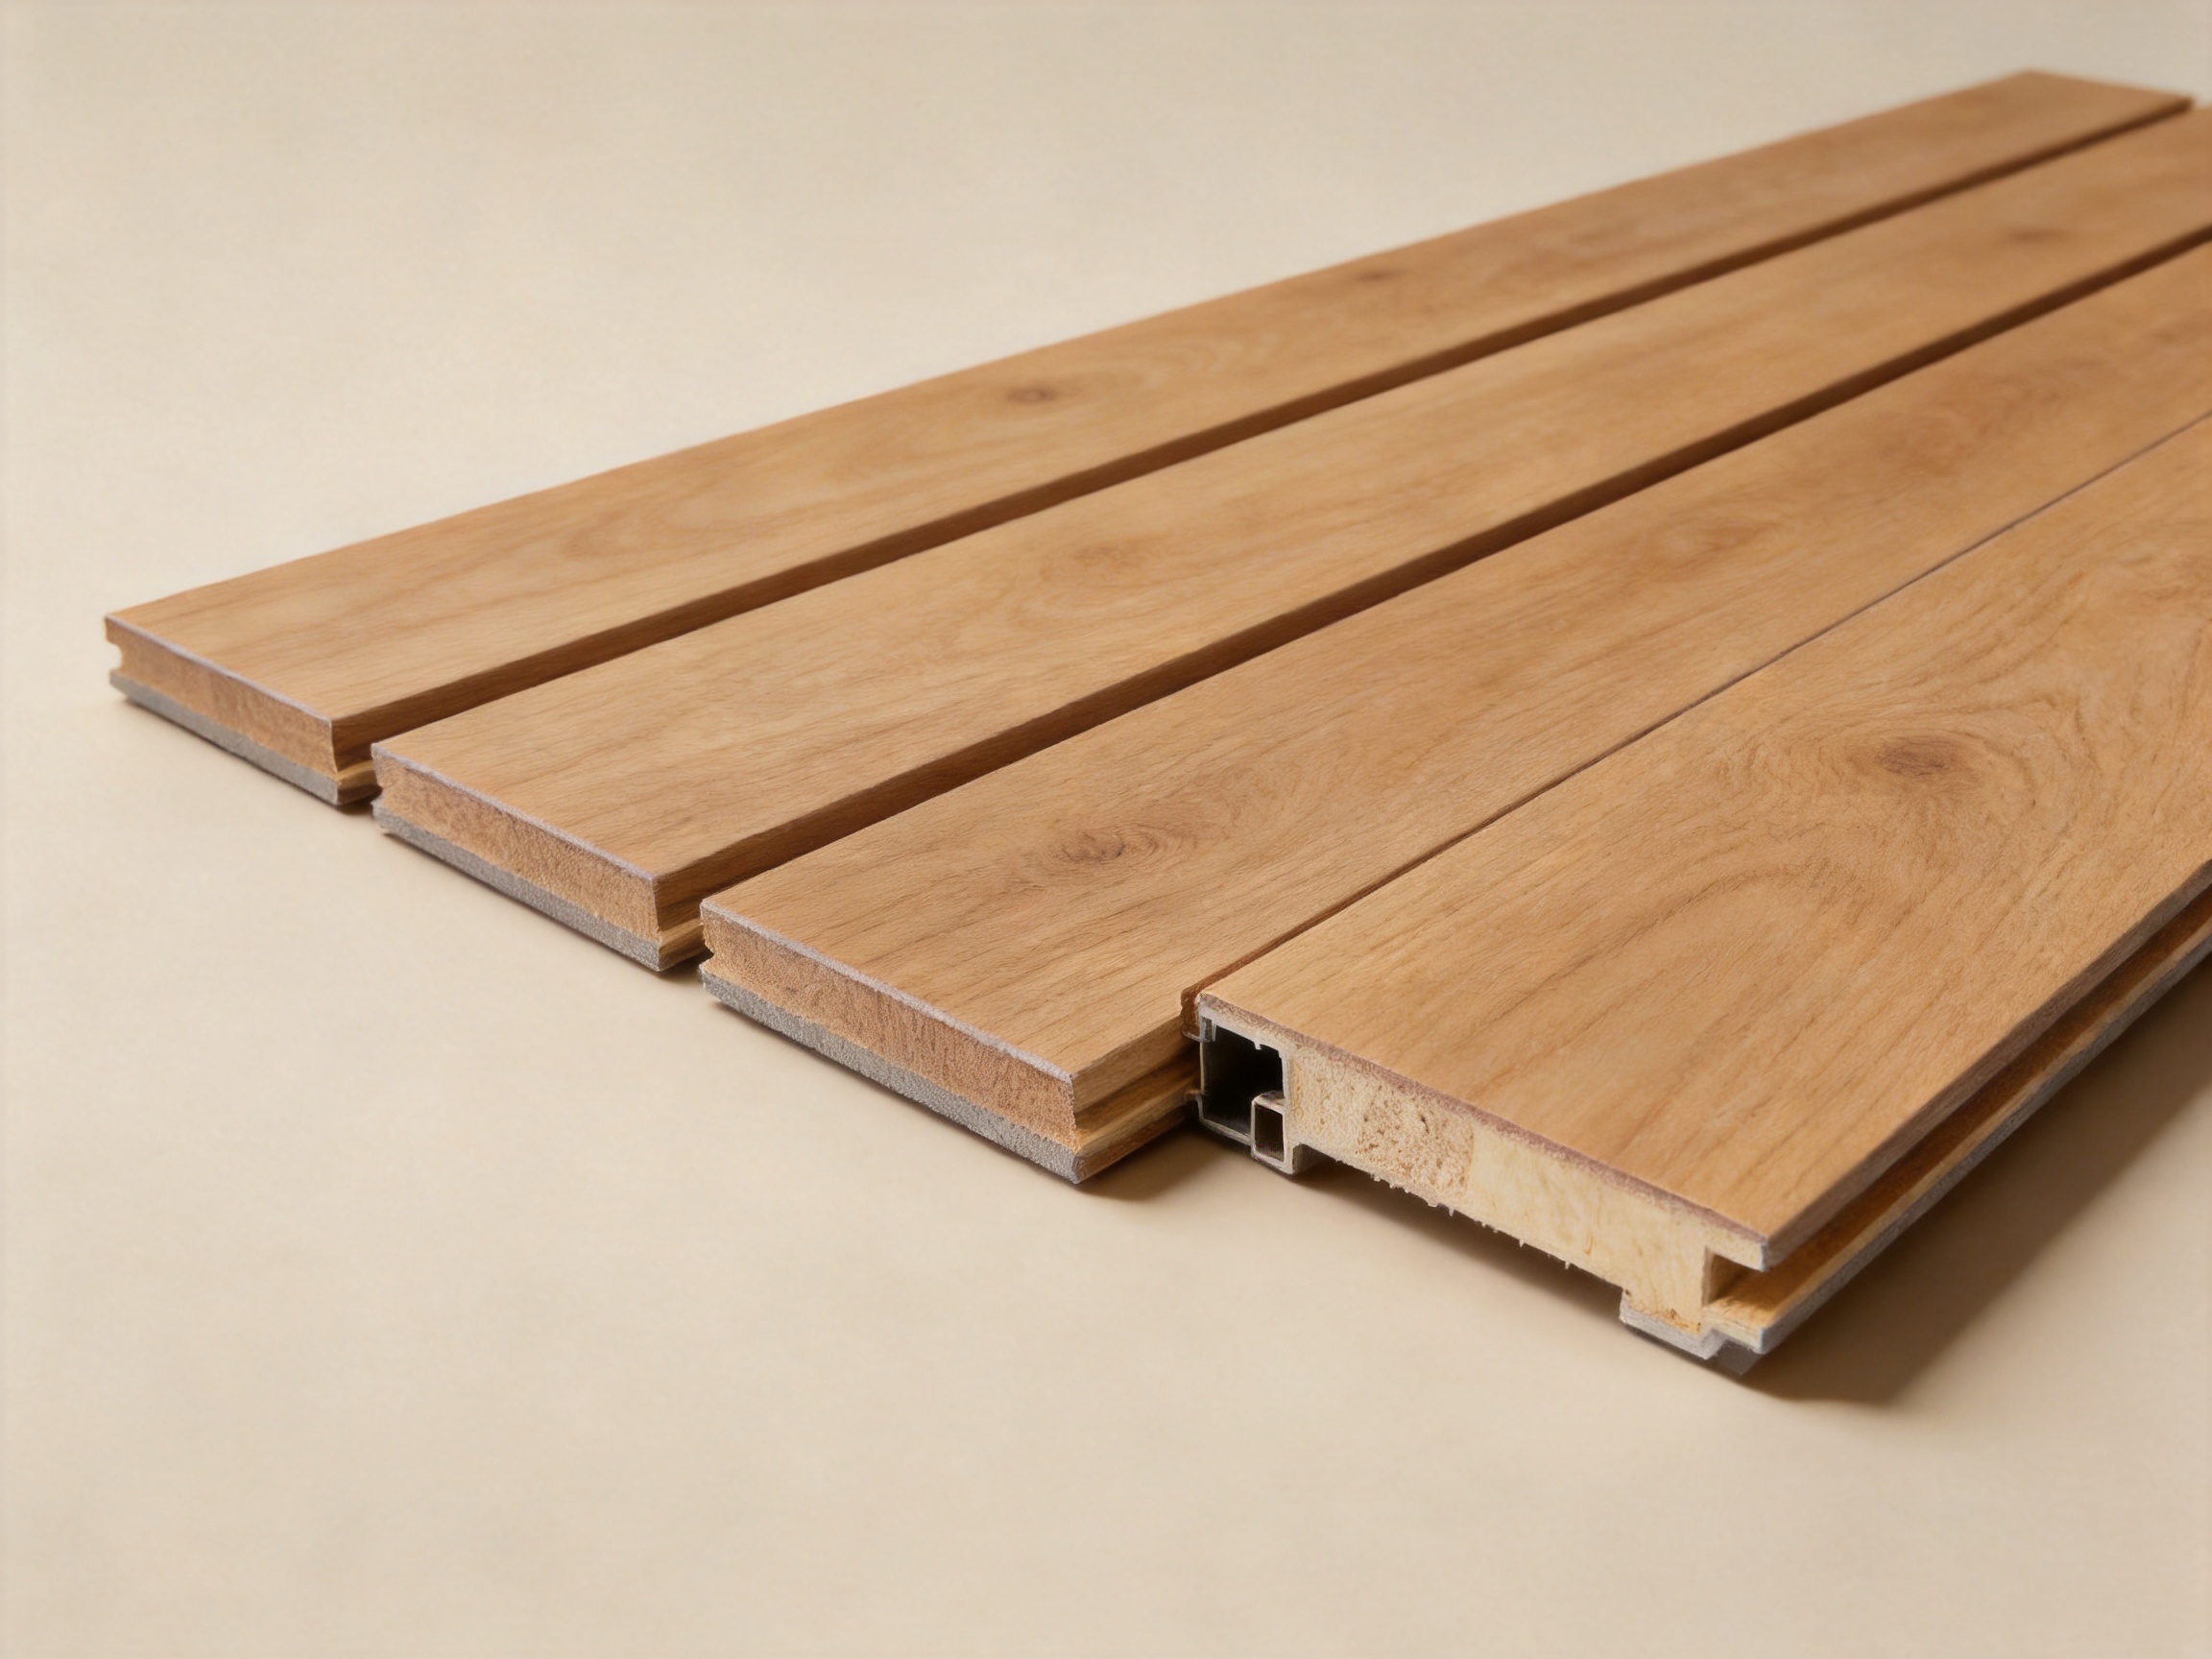
The product is designed with a natural wood veneer surface, a three-layer engineered wood core, a protective surface finish, and a four-sided micro-bevel. Its locking profile is suitable for click installation, while the board can also be installed using floating, glue-down, or stapled methods depending on the project requirements and subfloor conditions.
| Product Attribute | Specification |
| Product Code | DF-T1225 |
| Product Category | Three-layer engineered wood flooring |
| Standard Dimensions | 48.0 inches × 6.5 inches × 5/8 inch |
| Face Veneer | Customizable oak, walnut, ash, or teak |
| Standard Visual Direction | Light brown mountain grain appearance |
| Veneer Thickness | Customizable from 2 to 6 millimeters |
| Core Construction | Three-layer engineered wood |
| Core Material | Spruce or pine |
| Veneer Grade | Customizable AB, ABC, ABCD, or CD |
| Veneer Cut | Sliced veneer |
| Surface Finishes | UV lacquer, UV oil, or hardwax oil |
| Surface Textures | Wire brushed, hand scraped, or smooth sanded |
| Edge Profile | Micro-bevel on all four sides |
| Locking System | Click system |
| Installation Methods | Floating, glue-down, or stapled |
| Pieces Per Carton | 10 |
| Coverage Per Carton | 2.03 square meters or 21.85 square feet |
| Approximate Carton Weight | 24 kilograms |
The standard construction is suitable for general residential and commercial use, while customization makes the same product platform adaptable to different market segments. A buyer may specify the appearance, veneer thickness, grade, texture, finish, dimensions, and color according to the design brief, budget, and performance requirements.
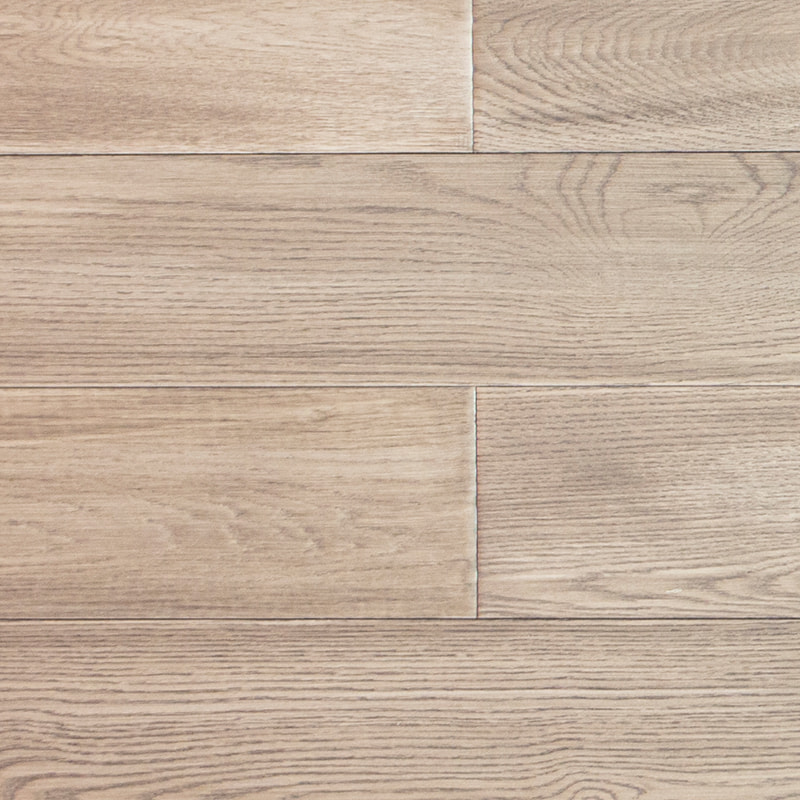
The defining visual characteristic of DF-T1225 is its light brown mountain grain pattern. The grain flows across the board in a natural, layered direction, creating movement while maintaining a calm and approachable appearance. Compared with very dark flooring, the light brown color can make rooms feel more open and brighter. Compared with extremely pale flooring, it adds greater warmth and visual depth.
This balanced color profile supports a wide range of interior palettes. It can be paired with white walls, pale textiles, natural stone, light-colored cabinetry, matte black fittings, brushed metal, or warm neutral furniture. In Nordic-inspired spaces, it reinforces the preference for daylight, clean lines, and natural materials. In Japanese-style interiors, it complements simple forms, low furniture, soft lighting, and a restrained material palette.
The mountain grain effect is also useful in projects that require a natural appearance without excessive variation. Designers can use the flooring as a consistent background for bedrooms, living rooms, dining spaces, guest rooms, offices, and boutique commercial environments. Its visual identity is distinctive enough to add character, yet sufficiently neutral to remain compatible with changing furniture and decoration styles.
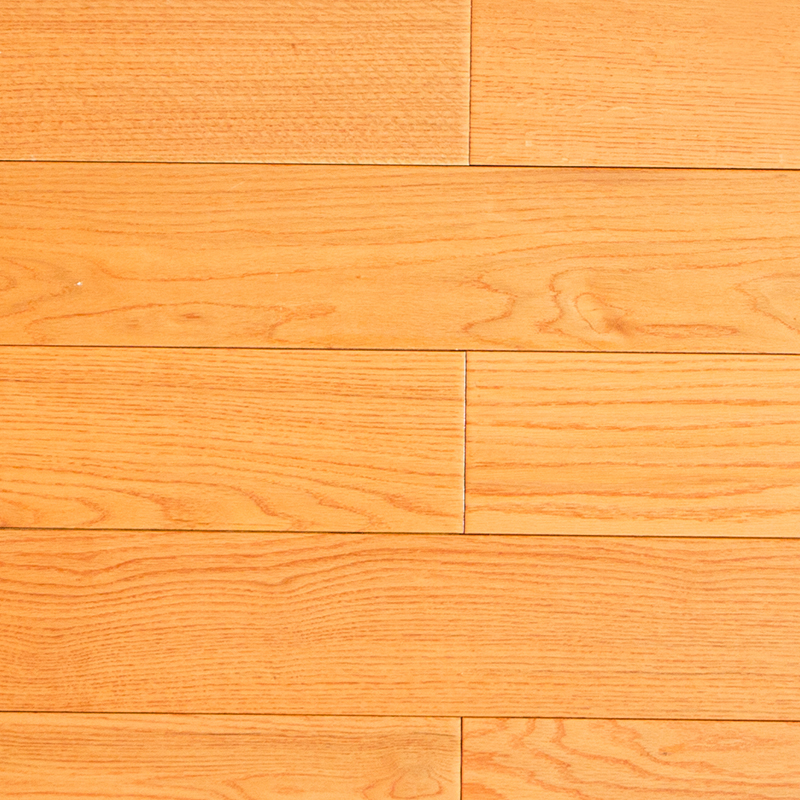
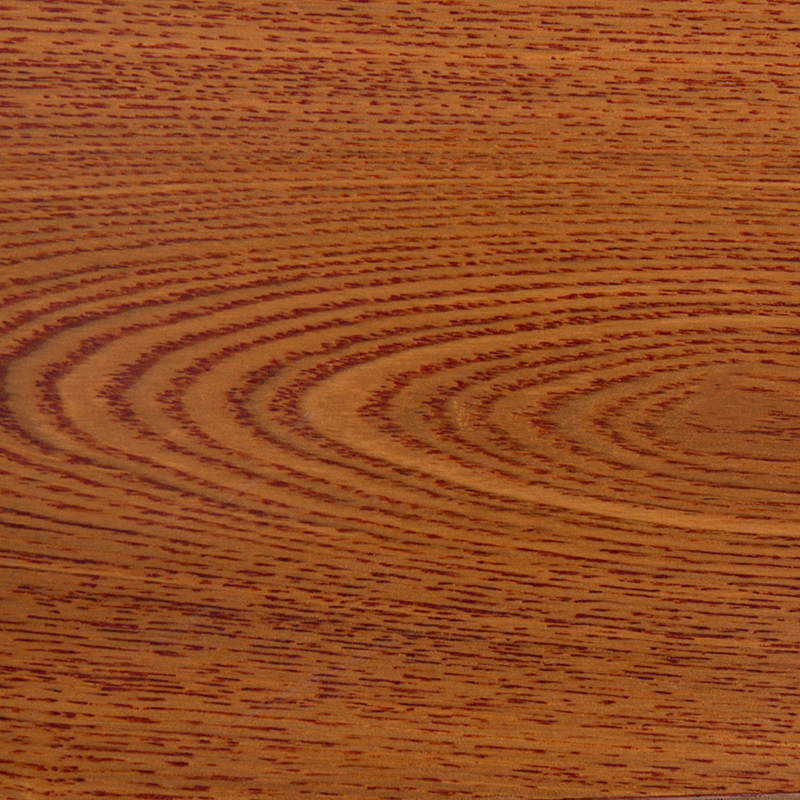
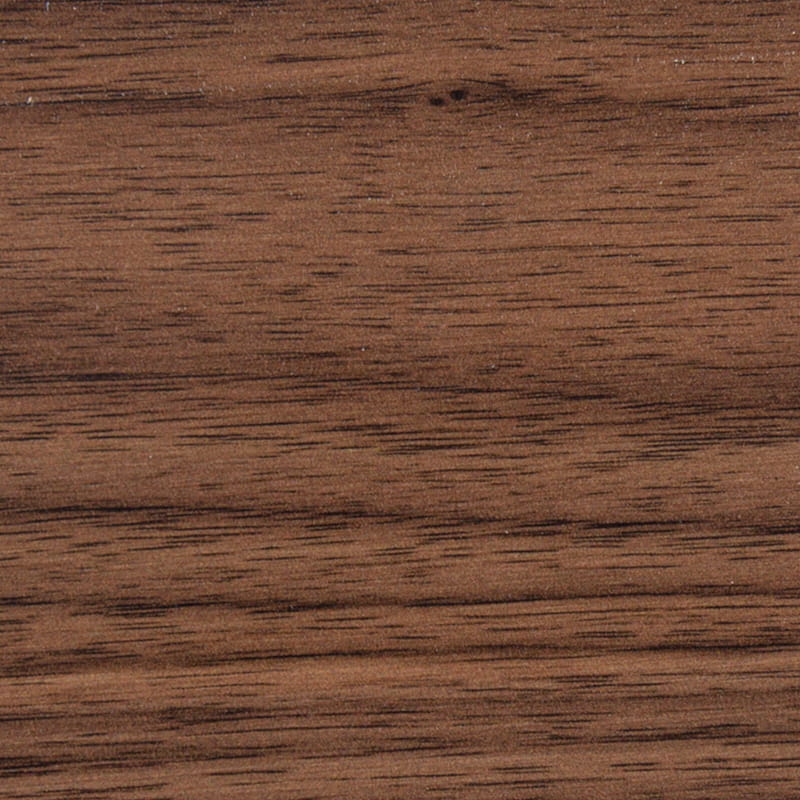
The standard veneer may be replaced with walnut, red oak, ash, teak, or other available options. This allows buyers to maintain the same basic engineered structure while adapting the surface to different markets and project concepts. Walnut can create a deeper and more luxurious atmosphere, while red oak provides a traditional and familiar wood expression. Ash may offer a lighter and more linear appearance, and teak can support warmer or more distinctive design schemes.
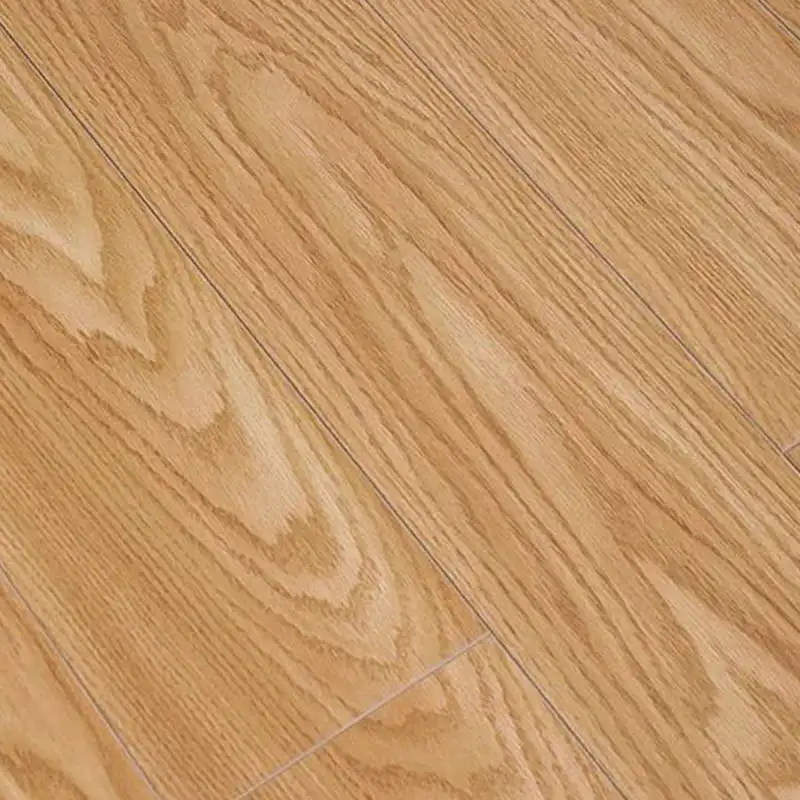
3-Layer Light Brown Mountain Grain Lock DIV Engineered Wood Flooring
One of the main advantages of engineered wood flooring is its layered construction. Instead of relying on a single piece of solid timber across the full thickness of the board, engineered flooring uses carefully arranged wood layers. In the three-layer design, the layers work together to improve dimensional control and reduce the tendency of the board to react dramatically to ordinary changes in temperature and humidity.
The core of DF-T1225 uses spruce or pine in a three-layer engineered configuration. The direction and arrangement of the layers help distribute internal stresses more evenly. This can reduce the risk of excessive expansion, contraction, warping, and cracking when the floor is properly transported, stored, installed, and maintained.
Solid wood flooring remains valued for its authenticity and ability to be refinished, but it can be more sensitive to environmental changes because the board is formed from one primary direction of timber grain. A three-layer engineered structure provides a more balanced construction. This makes the product a practical choice for projects where reliable dimensional performance is important.
Improved stability does not mean that the product is immune to moisture or unsuitable environmental conditions. Wood remains a natural material and must be protected from standing water, persistent dampness, and uncontrolled indoor climate changes. However, the engineered format offers a more controlled response than many traditional solid wood alternatives when used in appropriate interior applications.
The three-layer structure is particularly useful in rooms where the floor may experience regular changes in occupancy, temperature, or humidity. Bedrooms, dining areas, living rooms, guesthouse rooms, offices, and hospitality interiors can all benefit from a flooring system that combines natural appearance with predictable installation performance.
The engineered core provides several practical advantages. First, it helps limit the movement of individual boards. Second, it can improve the overall stability of the installed floor. Third, it supports a broad range of installation methods. Fourth, it allows the manufacturer to use a valuable natural veneer efficiently while maintaining an attractive finished product.
The core also helps create a consistent base for the surface veneer. When the base is properly manufactured and controlled, the finished boards can demonstrate better fit, more consistent appearance, and fewer installation complications. This is especially important in large projects where material consistency affects both labor efficiency and the final visual result.
For professional buyers, a stable three-layer construction may reduce the risk of avoidable delays associated with excessive board movement or inconsistent fit. For homeowners, it provides confidence that the floor is designed for everyday living rather than only for visual appeal.
DF-T1225 uses a sliced natural wood veneer surface. This means the visible layer retains the genuine grain, color variation, and tactile character of real wood. Natural veneer offers a more authentic appearance than printed decorative films or synthetic patterns, making it suitable for projects where material quality is a central part of the design concept.
The available veneer thickness can be customized from 2 to 6 millimeters. A thinner veneer can support cost-conscious projects and specific construction requirements, while a thicker veneer may be selected when a more substantial natural wood surface is preferred. The best choice depends on the intended application, product positioning, budget, and desired service life.
Veneer grade can also be adapted. Options include AB, ABC, ABCD, and CD grades. These grades generally allow buyers to select the level of natural variation, knots, color differences, and visual uniformity appropriate for the project. A more uniform grade may be preferred for modern residential interiors, premium hospitality spaces, or projects seeking a clean, refined appearance. A more character-rich grade may be suitable for rustic, country, vintage, or naturally expressive environments.
The ability to choose veneer grade gives distributors greater flexibility when serving different customer groups. Instead of offering only one appearance and quality level, a supplier can develop multiple product positions from the same core platform. This helps support entry-level, mid-range, and premium collections while maintaining a consistent manufacturing relationship.
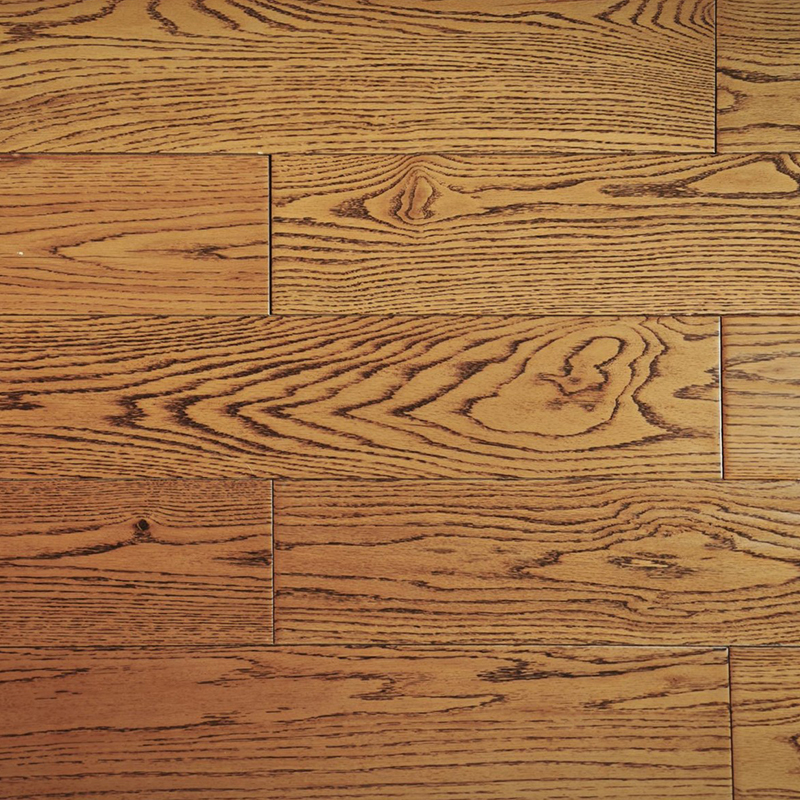
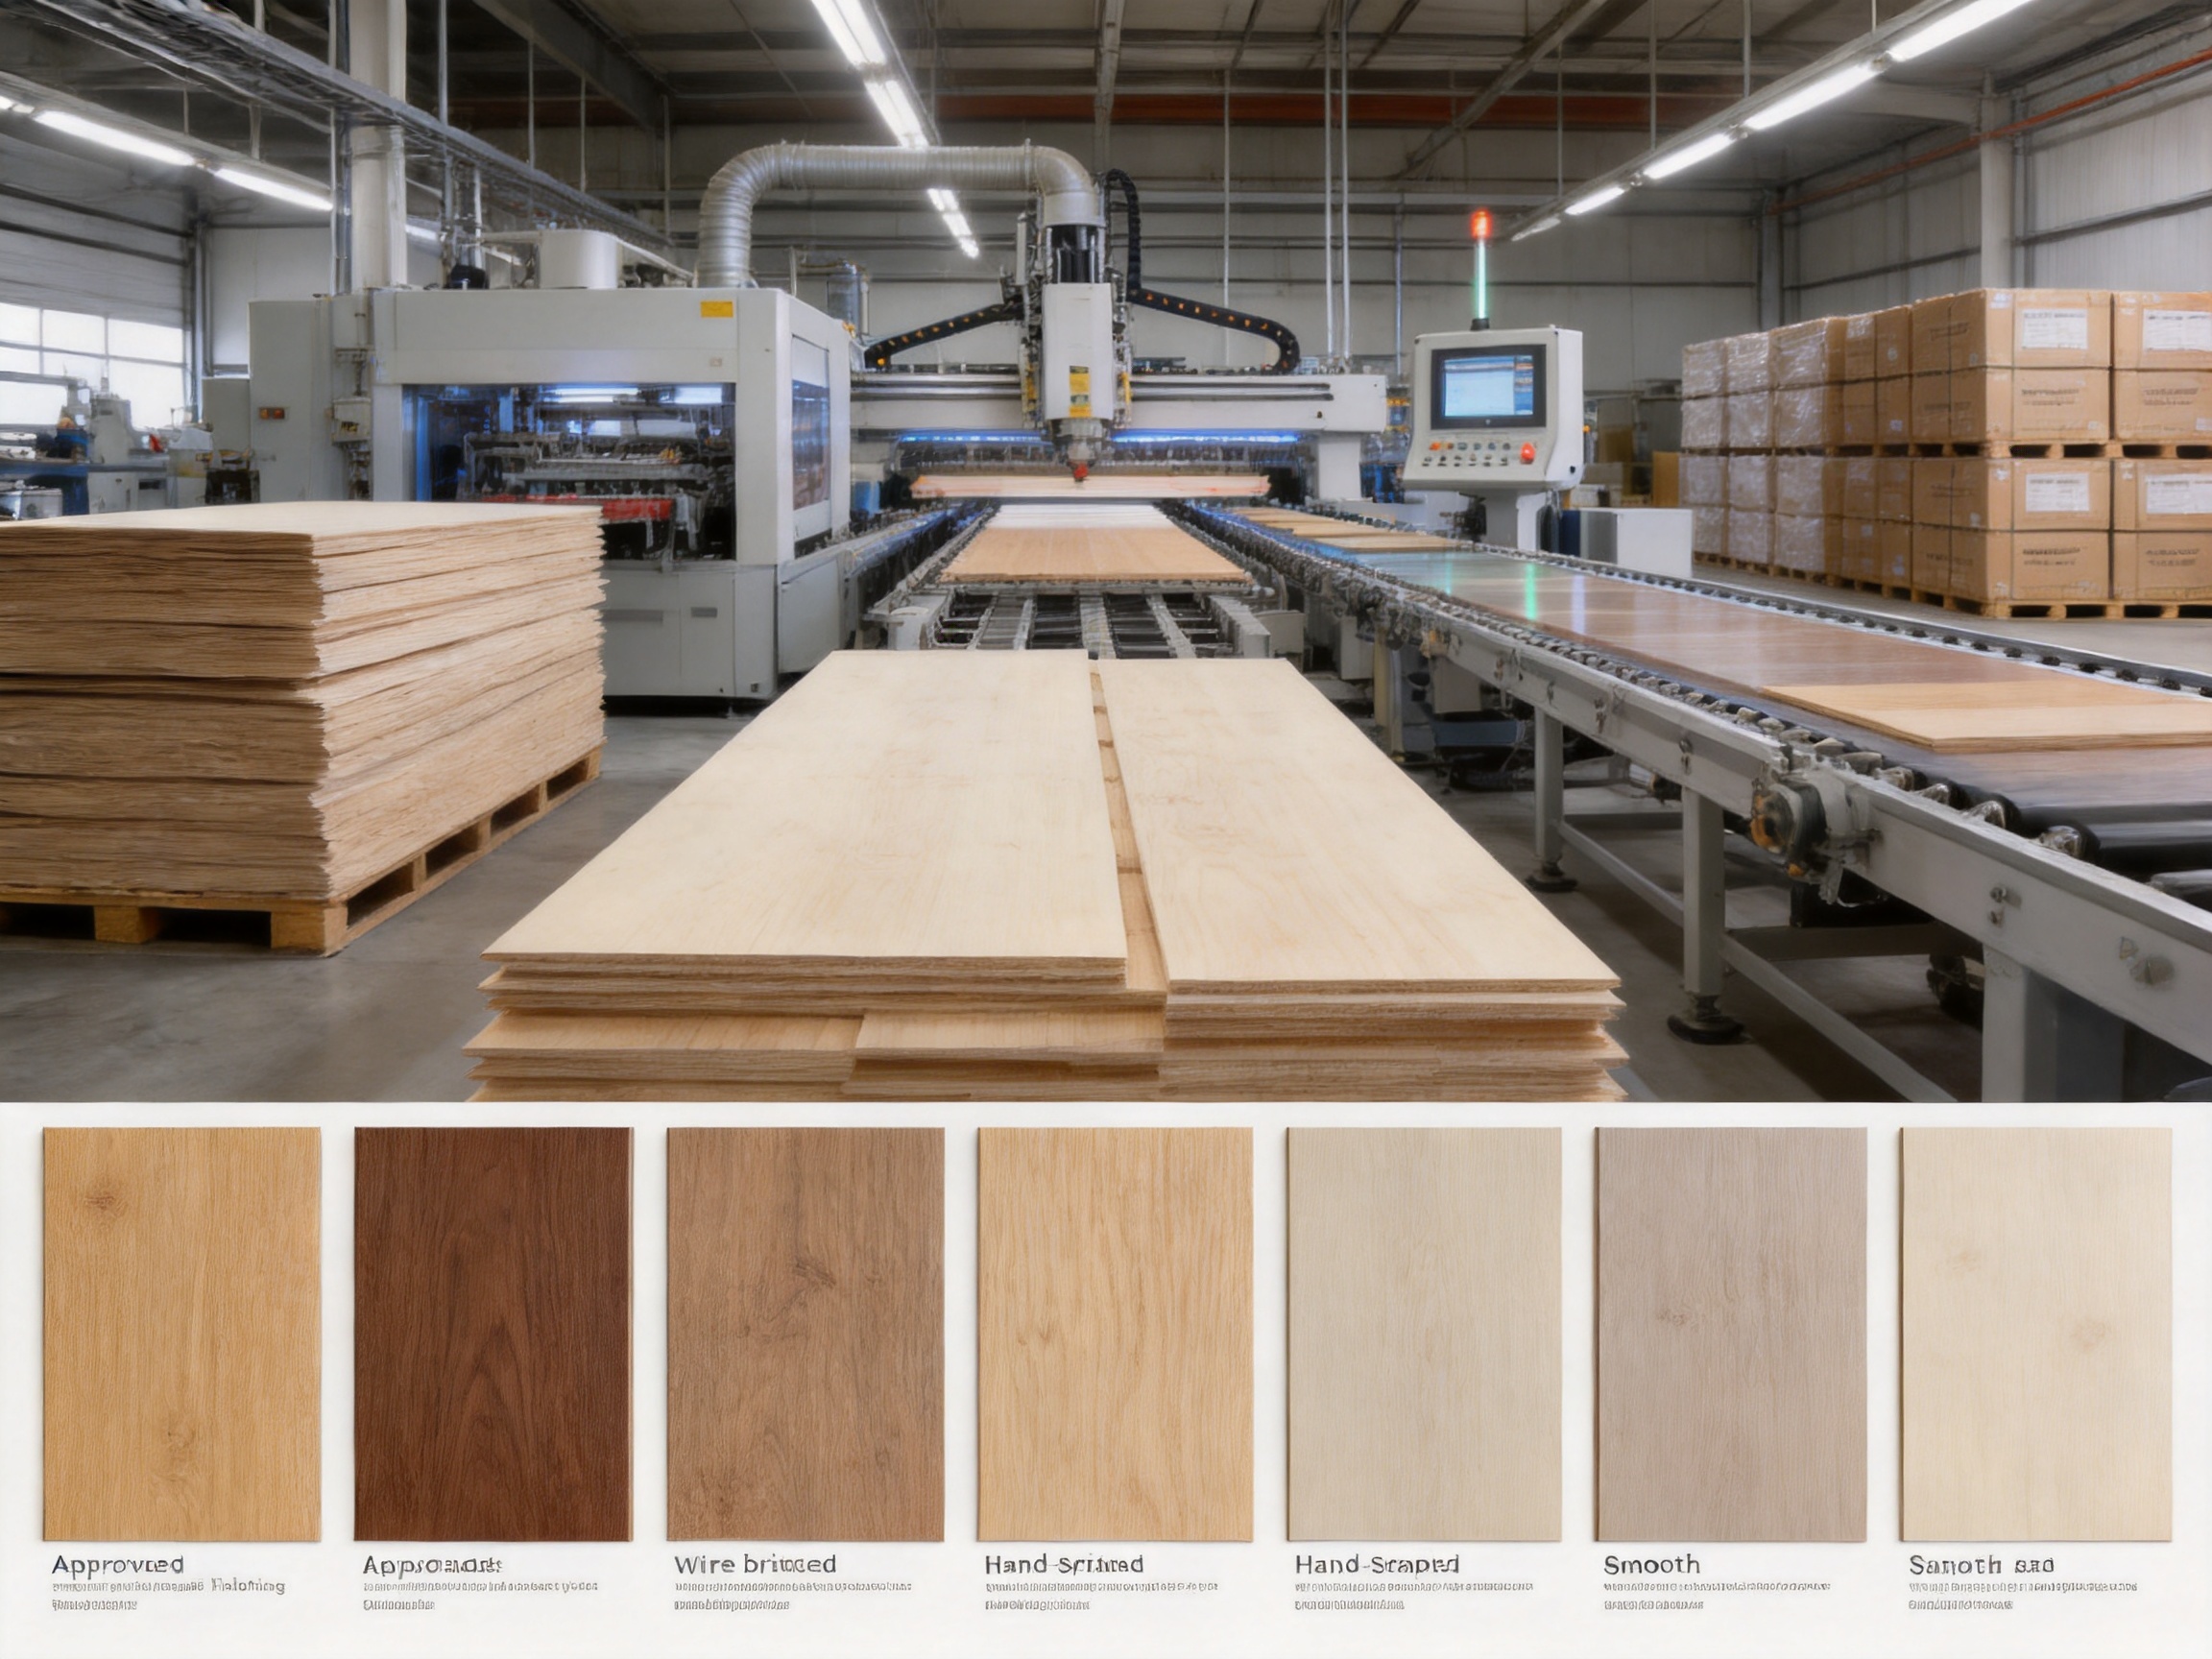
The surface can be customized with wire brushing, hand scraping, or smooth sanding. Wire brushing emphasizes the softer grain areas and creates a tactile, lightly textured surface. It is often selected for natural, Scandinavian, farmhouse, and contemporary interiors. Hand scraping produces a more expressive, handcrafted appearance and can add visual depth to rustic or heritage-inspired spaces.
Smooth sanding creates a cleaner and more understated surface. It can be suitable for minimalist interiors, modern apartments, professional offices, and projects where furniture and architectural details provide the main visual emphasis. The choice of texture also affects how light interacts with the floor, how the grain is perceived, and how small marks may appear during daily use.
These texture options demonstrate that DF-T1225 is not limited to one fixed style. It can be adapted to different markets while preserving the key advantages of a natural wood veneer and a stable engineered core.
The flooring can be finished with UV lacquer, UV oil, or hardwax oil. Each finishing direction offers a different balance of appearance, tactile quality, maintenance expectations, and project positioning.
UV lacquer creates a protective film over the wood surface and is widely used for flooring that requires practical resistance to everyday wear and scratching. The product information identifies a seven-layer UV coating system for general use. This layered finishing approach is intended to strengthen the surface and help protect the decorative veneer during normal interior use.
UV oil provides a different visual and tactile effect. It can preserve a more natural-looking appearance while adding surface protection. Hardwax oil is often chosen when a warm, low-sheen, natural-touch finish is desired. The appropriate finish should be selected according to the expected traffic level, cleaning routine, visual concept, and maintenance plan.
A protective finish does not eliminate the need for responsible care. Sharp objects, dragging furniture, abrasive particles, excessive moisture, and unsuitable cleaning chemicals can damage any wood floor. Nevertheless, a properly applied finishing system gives the floor a valuable first line of defense against common household and commercial wear.
Compared with unfinished boards or products with minimal surface treatment, a professionally finished engineered floor can offer more consistent appearance and easier day-to-day maintenance. The seven-layer UV coating option supports a durable product position for residential and light commercial spaces where the floor must remain attractive under regular use.
The finish also helps reduce the amount of immediate site work required after installation. Factory finishing provides a more controlled appearance than applying coatings under variable jobsite conditions. It can help improve consistency from board to board and reduce the time between installation and occupancy.
The Lock DIV system is designed to support fast and efficient installation. Click flooring systems allow boards to connect through a precision-machined profile, reducing the need for extensive on-site fastening or wet adhesive work in suitable floating installations. This can be particularly valuable in renovation projects, hospitality rooms, offices, and commercial spaces where time on site directly affects cost and scheduling.
The product includes a click system and a micro-bevel on all four sides. The four-sided micro-bevel helps define individual boards and can create a refined plank appearance after installation. It may also provide a subtle transition between adjacent boards, emphasizing the floor’s natural linear layout.
DF-T1225 supports floating, glue-down, and stapled installation methods. The most appropriate method depends on the subfloor, acoustic requirements, room conditions, local construction practices, and project specifications. A floating installation may support speed and easier replacement. Glue-down installation can provide a more solid underfoot feel and may be selected for particular subfloor or acoustic needs. Stapled installation may be considered where the construction system and subfloor are suitable.
Before installation, the product should be inspected, acclimatized according to professional flooring practice, and installed over a properly prepared subfloor. The subfloor should be clean, dry, stable, level, and structurally sound. Expansion allowances should be included where required, and installation should follow the approved technical instructions for the selected method.
Compared with traditional site-finished solid wood flooring, the click format and factory-finished surface can reduce installation complexity. Contractors may spend less time on sanding, coating, and curing, while building owners may be able to return spaces to service more quickly. These advantages are especially meaningful in guesthouses, short-term rental properties, retail fit-outs, and commercial renovations.
The light brown tone is particularly well suited to bedrooms. It creates a comfortable and calm atmosphere that works with both contemporary and traditional furniture. When combined with natural textiles, warm lighting, and simple wall colors, the floor can make a bedroom feel more relaxed and connected to nature.
Living rooms are another natural application. The mountain grain gives the floor enough character to become an architectural feature, while the moderate color prevents it from dominating the space. The floor can be coordinated with sofas, shelving, rugs, and wood furniture in both light and medium tones.
In dining rooms, the engineered structure offers a practical balance of appearance and stability. Dining areas often experience repeated movement, chair traffic, food particles, and occasional spills. Proper surface protection and routine care are therefore important. With sensible maintenance and moisture control, the floor can provide an attractive and durable dining environment.
Home offices, hallways, studies, and open-plan interiors can also benefit from the product’s flexible visual character. It can connect different functional zones and create continuity across a residential layout. The standard plank size provides a familiar wood-floor proportion, while custom dimensions may be considered for projects requiring a particular visual rhythm.
DF-T1225 is also suitable for selected commercial applications. Guesthouse rooms, boutique hotels, serviced apartments, offices, model homes, private clinics, and low- to medium-traffic retail interiors may benefit from its natural appearance and efficient installation format.
Guesthouse and hospitality rooms often require a combination of visual warmth, predictable supply, and fast installation. A natural wood floor can make a room feel more comfortable and distinctive than a purely synthetic surface. At the same time, the click system and factory finishing can help contractors complete rooms according to a tight schedule.
For commercial developers, the ability to customize veneer, color, surface texture, and finish provides an opportunity to create a consistent design identity across multiple properties. A hospitality group may select a warm walnut variation for premium rooms, a light oak-inspired design for standard rooms, or a brushed finish for a more relaxed boutique concept.
In offices and professional interiors, the light brown color can soften the appearance of glass, metal, and painted surfaces. It can contribute to a more welcoming environment without reducing the clean, organized impression expected in a workplace. In display apartments and showrooms, natural veneer helps communicate quality and lifestyle value to prospective buyers.
Commercial buyers should match the selected finish and maintenance program to the expected traffic level. Areas receiving heavy rolling loads, substantial moisture, or demanding industrial use may require a different flooring specification. DF-T1225 is best evaluated within the performance needs of the specific project rather than treated as a universal solution for every commercial environment.
When compared with basic laminate products, DF-T1225 offers the authentic visual and tactile qualities of a natural wood veneer. Laminate flooring can provide useful durability and design flexibility, but its decorative surface is generally a printed image rather than a real wood layer. For buyers who value genuine material character, engineered wood provides a more natural alternative.
When compared with solid wood flooring, the three-layer structure can provide improved dimensional control and greater installation flexibility. Solid wood remains attractive for certain applications, especially where substantial refinishing potential is required, but it may respond more noticeably to environmental changes. The engineered structure can be more practical for projects seeking stability and a faster installation process.
When compared with thin veneer products, DF-T1225 offers customizable veneer thickness, including options up to 6 millimeters. This allows product specifications to be aligned with intended use and market positioning. The availability of multiple grades and surface textures further expands the range of possible finished products.
When compared with flooring that is finished entirely on site, factory-applied UV lacquer, UV oil, or hardwax oil can provide more consistent finishing quality and reduce jobsite preparation. A factory-controlled process can also support more predictable production, packaging, and quality inspection.
The main competitive advantage is therefore not one single feature. It is the combination of authentic natural veneer, a stable three-layer core, protective finishing, customization, efficient click installation, and professional manufacturing support.
Suzhou Dicosbo Wood Co., Ltd. is a wood solutions manufacturer specializing in wood flooring, wooden doors, and custom cabinet products. Established in 1999, the company has more than two decades of experience in wood manufacturing and over ten years of export experience.
The company operates production facilities covering approximately 20,000 square meters. Its reported annual production capacity includes approximately 2,400,000 square meters of flooring and 5,000 sets of doors. This capacity supports both standard orders and project-based requirements, subject to production scheduling, material availability, and approved specifications.
German imported production lines and automated quality control systems are used to support manufacturing consistency. For engineered flooring, consistency is important at every stage, including veneer preparation, core assembly, bonding, machining, sanding, surface finishing, profiling, inspection, and packing.
Modern production equipment can help maintain accurate board dimensions and stable locking profiles. This is especially relevant for click flooring, because even small variations in profile geometry can affect installation efficiency and finished-floor appearance. Automated control systems also support repeatability across larger orders and multiple production batches.
The company applies a three-step quality inspection process. While the exact internal checkpoints may vary by order and product specification, a structured inspection approach commonly includes raw material evaluation, in-process production control, and final finished-product inspection.
Raw material inspection helps verify the condition and suitability of veneer, core timber, adhesives, and finishing materials. In-process inspection can monitor construction quality, bonding, dimensions, moisture-related conditions, surface treatment, and profile accuracy. Final inspection can assess appearance, packaging, quantity, labeling, and compliance with the approved sample or technical requirements.
This structured approach is valuable for international buyers because project success depends on more than visual design. Material consistency, dimensional accuracy, packaging protection, documentation, and repeatability all influence the total cost and performance of a flooring order.
The company offers OEM and ODM customization, with rapid prototyping reported at approximately 72 hours for suitable development requests. Rapid prototyping can help buyers evaluate a new color, veneer, surface treatment, texture, or profile before committing to a larger production run.
For architects and design studios, this service can shorten the time between concept development and material approval. For distributors, it can support the creation of exclusive collections. For developers and contractors, it can help align flooring appearance with a broader interior specification.
Prototype timing depends on the complexity of the requested product, material availability, approval requirements, and production workload. Nevertheless, the capability demonstrates a manufacturing model designed to support more than standard catalog sales.
The product information identifies EU CE and FSC certification for applicable product lines and general use. The company also reports compliance or support for CARB Phase 2 and ISO 9001 requirements. These standards and certifications are important to international buyers because they provide a framework for evaluating product conformity, responsible sourcing, quality management, and emissions-related expectations.
FSC certification is associated with responsible forest management and chain-of-custody practices when the certified claim applies to the specific product and order. Buyers should confirm the relevant certificate scope, product claim, and documentation before making project-wide compliance statements.
CE marking may be relevant to applicable European product requirements. The exact requirements depend on the product category, intended market, and applicable technical standards. Professional buyers should review declarations, test reports, and technical documentation with their project consultants or compliance teams.
CARB Phase 2 is associated with limits on formaldehyde emissions from composite wood products in applicable markets. ISO 9001 relates to quality management systems and process control. Together, these compliance references can support more informed procurement, particularly for projects involving public buildings, international developers, and environmentally conscious clients.
Each carton contains 10 pieces and covers approximately 21.85 square feet. This standardized packing information helps buyers estimate quantities, shipping volume, installation waste, and warehouse requirements. Final ordering should include an appropriate allowance for cutting, layout selection, repairs, and future replacement boards.
For large projects, flooring should be coordinated with the construction schedule. Delivery timing should account for production, inspection, packaging, export procedures, inland transportation, ocean or air freight, customs clearance, and final delivery. The product’s factory-finished surface can help reduce some site activities, but proper storage and acclimatization remain essential.
Cartons should be stored in a dry, protected, and appropriately ventilated location. They should be kept flat and protected from direct water exposure. Storage conditions should be reviewed with the installer and project manager, especially when the flooring will be installed in a region with significant seasonal humidity changes.
For international distribution, accurate product documentation is also important. Technical data should clearly identify dimensions, construction, veneer species, veneer thickness, finish, texture, locking system, packaging, and installation recommendations. Consistent documentation helps distributors train customers and reduces the risk of specification errors.
Routine maintenance for DF-T1225 is straightforward when the floor is protected from excessive moisture and abrasive contamination. Dry mopping or vacuuming with a suitable floor attachment can remove dust, sand, and loose particles. These particles should be removed regularly because they may act as abrasives under footwear and furniture.
Spills should be cleaned promptly with a slightly damp cloth or an appropriate wood-floor cleaning product. Standing water should not be allowed to remain on the surface. Wet mopping with excessive water, steam cleaning, or harsh chemicals may damage the finish or contribute to moisture-related movement.
Sharp objects and heavy furniture should be handled carefully. Felt pads can be placed under chair legs, tables, sofas, and other movable furniture. Heavy items should be lifted rather than dragged. Entrance mats can help reduce the amount of grit brought into the room.
Indoor humidity should remain within a moderate and stable range appropriate for wood flooring. Sudden and extreme changes in humidity can affect any natural wood product, even when it has an engineered construction. Heating and cooling systems should be operated in a way that avoids prolonged environmental extremes.
Maintenance requirements may vary according to the selected finish. UV lacquer, UV oil, and hardwax oil should each be maintained using products compatible with the factory finish. Before applying any cleaning or maintenance chemical, users should review the product instructions and, when necessary, test it in an inconspicuous area.
When selecting DF-T1225 for a project, buyers should first define the intended application. Residential bedrooms, dining rooms, guesthouse rooms, offices, and display spaces may have different priorities for texture, finish, grade, and installation method.
The next consideration is the visual direction. The light brown mountain grain is suitable for warm and natural interiors, but the same construction can be customized with walnut, red oak, ash, teak, or other approved veneer options. The chosen species should be evaluated together with wall colors, cabinetry, doors, furniture, lighting, and the overall architectural concept.
Veneer thickness and grade should be selected according to the desired product position. A thicker veneer and premium grade may support a higher-end collection, while a more economical specification may be appropriate for volume residential development or rental properties.
Surface texture should be selected with both appearance and maintenance in mind. Wire brushing and hand scraping can emphasize character and disguise minor visual variation, while smooth sanding offers a cleaner and more refined look. The surface finish should reflect the expected traffic, desired sheen, tactile quality, and maintenance resources available to the owner.
Finally, the installation method should be confirmed with the installer. The subfloor, room dimensions, acoustic targets, underlayment, moisture conditions, and local building practices all influence the correct installation approach.
DF-T1225 uses a three-layer engineered wood construction rather than a single solid timber board. The layered structure helps improve dimensional stability and reduce the risk of excessive movement caused by ordinary environmental changes. It also supports multiple installation methods and can be supplied with a factory-applied protective finish.
Yes. The product uses a sliced natural wood veneer surface. The standard visual direction is a light brown mountain grain appearance, and the veneer can be customized with options such as oak, walnut, ash, or teak, subject to availability and order specifications.
Yes. Veneer thickness can generally be customized from 2 to 6 millimeters. The final selection should be based on the project’s design requirements, budget, product positioning, and intended application.
Available options include UV lacquer, UV oil, and hardwax oil. UV lacquer is commonly selected for practical surface protection, while UV oil and hardwax oil can provide different visual and tactile effects. The appropriate finish depends on traffic, maintenance expectations, and the desired appearance.
The available texture options include wire brushed, hand scraped, and smooth sanded. Each creates a different visual and tactile result, allowing the floor to be adapted to modern, Nordic, rustic, traditional, or minimalist interiors.
Yes, a floating installation may be possible using the click system when the subfloor and project conditions are suitable. The product can also be installed with glue or staples when those methods are appropriate for the construction and approved by the flooring professional.
Yes. Its stable three-layer structure and protective finishing make it suitable for dining rooms and similar residential spaces. Spills should be cleaned promptly, excessive moisture should be avoided, and routine dry cleaning should be performed.
It can be suitable for selected commercial applications such as guesthouse rooms, serviced apartments, offices, model homes, boutique interiors, and other spaces requiring natural appearance and efficient installation. The final specification should be matched to the expected traffic and maintenance program.
The click system is designed to connect boards efficiently and can help reduce installation time. It is especially useful for renovation and project environments where rapid completion is important. Installation still requires a properly prepared subfloor and compliance with professional flooring procedures.
Regular dry mopping or vacuuming with a suitable attachment is recommended. Spills should be wiped promptly, and excessive water, steam cleaning, abrasive products, and harsh chemicals should be avoided unless specifically approved for the selected finish.
The product information identifies EU CE and FSC certification for applicable general-use product lines. The company also reports support for CARB Phase 2 and ISO 9001 requirements. Buyers should request current certificates and verify that the documents apply to the specific product, material claim, and order.
Yes. OEM and ODM services are available, and rapid prototyping may be offered for suitable requests. Custom development can include veneer species, color, grade, thickness, texture, finish, dimensions, and other approved specifications.
The 3-Layer Light Brown Mountain Grain Lock DIV Engineered Wood Flooring is designed to combine the natural appeal of genuine wood with the practical advantages of engineered construction. Its light brown mountain grain surface creates a warm and versatile visual foundation for residential and commercial interiors, while the three-layer spruce or pine core helps improve stability and reduce deformation.
Its competitive value comes from the complete system: natural veneer, customizable thickness and grade, multiple surface finishes, optional textures, four-sided micro-beveling, click installation, and several approved installation methods. These features allow the product to serve different design styles and project requirements without sacrificing the essential character of real wood.
Manufacturing capability further strengthens the product proposition. Suzhou Dicosbo Wood Co., Ltd. combines long-term industry experience, substantial production facilities, German imported production lines, automated quality control, OEM and ODM support, rapid prototyping, and a structured three-step inspection process. Its reported capacity and international compliance support make the company a suitable partner for distributors, architects, contractors, developers, and project buyers seeking stable wood flooring supply.
With correct specification, professional installation, responsible moisture control, and routine care, DF-T1225 can provide a durable and attractive flooring solution for bedrooms, dining rooms, living areas, guesthouse rooms, offices, and other interior applications. It offers the warmth of natural wood, the control of engineered construction, and the flexibility required by modern global projects.
1. Product Technical Data Sheet for DF-T1225, three-layer engineered wood flooring specification.
2. Manufacturer-provided information regarding veneer options, core construction, surface finishes, locking systems, packaging, and installation methods.
3. General professional guidance on engineered wood flooring installation, acclimatization, subfloor preparation, and maintenance.
4. European conformity and product documentation principles applicable to CE-marked construction and interior materials.
5. Forest stewardship and chain-of-custody principles associated with FSC-certified wood products.
6. Formaldehyde emission requirements associated with CARB Phase 2 composite wood product regulations.
7. ISO 9001 quality management system principles for manufacturing organizations.
We provide customers with sustainable and eco-friendly
engineered wood solutions and services.
Choose DEIF for the perfect blend of
performance and aesthetics.
